
L'ovalità del tubo e la rettilineità della linea centrale sono condizioni geometriche diverse. L'ovalità riguarda la forma di una sezione trasversale; la rettilineità dell'asse riguarda il percorso del tubo lungo la sua lunghezza. Un tubo può avere una geometria della linea centrale accettabile ma essere fuori circonferenza in una stazione, oppure può essere rotondo in ogni sezione misurata mentre la sua linea centrale si piega su una lunga campata. Trattare queste condizioni come un unico valore di “rettilineità” può portare a una decisione sbagliata sul processo.
Questa guida è un quadro di misurazione e accettazione. Non rivendica una gamma di tubi StraighteningTech, capacità del muro, misura, sensore, tolleranza o processo di correzione convalidato. I requisiti finali devono provenire dal disegno controllato, metodo di riferimento e campioni rappresentativi.

*Illustrazione del concetto di ingegneria. Descrive il contesto del processo di raddrizzamento dei tubi, non è una prova che una specifica famiglia di tubi o condizioni di parete possano essere lavorate.*
Define Each Characteristic Before Measuring Either
Ovality is a per-station property: every measured cross-section has its own value, and a tube inspected at twelve stations has twelve ovality values that can differ. Centerline straightness is a whole-length property: it is derived from the path traced by the successive centers of those cross-sections. The two characteristics do not merely describe different defects — they live at different levels of the measurement chain, and the higher level is computed from the lower one.
That dependency is the hidden coupling. A centerline is not measured directly; it is computed, station by station, from sections that are never perfectly round. Whichever rule converts a measured section into a single center point — the average of two diameters, il centro di un cerchio dei minimi quadrati, un centro del cerchio di zona minima, oppure il centro segnalato da un misuratore a due punti, diventa parte della definizione di rettilineità. Due metodi di ispezione possono quindi non essere d'accordo riguardo alla linea centrale dello stesso tubo fisico pur essendo ciascuno internamente coerente, perché incorporavano regole diverse per la ricerca del centro.
I documenti di accettazione dovrebbero indicare, per ogni caratteristica: la formula (ovalità basata sul diametro, ovalità basata sulla deviazione radiale, o una tolleranza della forma completa), la regola di ricerca del centro che alimenta il calcolo della linea centrale, e il set di stazioni su cui si applica ciascun valore. Un singolo “rettilineità OK” la registrazione che non indica quali regole hanno prodotto non è trasferibile tra misuratori fornitore e cliente.
Measure Cross-Section and Lengthwise Geometry With Appropriate Supports
Support positions can affect the apparent centerline through sag; il bloccaggio può influenzare una sezione a parete sottile; il contatto della sonda può influenzare la risposta della superficie o della parete. La procedura dovrebbe quindi definire le condizioni per ciascuna caratteristica e ripetere/ripristinare i controlli ove necessario.
| Controllo della misurazione | Perché è importante |
|---|---|
| Stazione e orientamento della sezione trasversale | L'ovalità può variare lungo la lunghezza e attorno alla circonferenza |
| Campata longitudinale e appoggi | Centerline readings can include gravity and fixture effects |
| Condizione di riferimento e finale | Determina se il risultato si riferisce alla funzione prevista |
| Contatto o metodo ottico | Può introdurre superfici diverse, Limiti di accesso e di incertezza |
| Condizione rilasciata | Impedisce che il vincolo temporaneo venga segnalato come geometria finale |
Spaziatura supporto Filtra il segnale della linea centrale
Su un arco misurato, supports act as a mechanical filter for the centerline reading: bending content with a wavelength shorter than the support spacing is partially suppressed by the stiffened sections, while longer-wavelength bow passes into the reading. The same tube can therefore report different bow on a short fixture span than on a long one without either reading being wrong. The support span is not a setup convenience — it is part of the straightness definition, and it must match, or be explicitly correlated to, the span used by the customer gauge.
Station spacing plays the analogous role in the sampling domain. Widely spaced stations under-sample the centerline path and can miss a local kink between stations; very dense stations begin to mix surface and wall-thickness variation into the computed axis. The sampling plan should state where stations sit — not only how many — because the informative stations are the support points, the clamping points, the tube ends and the neighborhoods of expected bend peaks.
On thin-wall tubes the supports carry a second, unwanted effect: support reaction can ovalize the section locally, so the ovality measured at a support station includes a measurement-induced contribution. Comparing readings at supported stations against readings taken just outside the support influence is a cheap check for this; where the difference is significant, the ovality acceptance must be evaluated at defined free stations. For the loaded-versus-released distinction in final acceptance, Vedere misurazione della rettilineità caricata o rilasciata.
Non correggere un errore e dare per scontato che l'altro sia risolto
Un processo di correzione inteso a ridurre l'arco può modificare l'ovalità o la condizione della parete. Un processo inteso a migliorare la forma della sezione potrebbe non stabilire la rettilineità della linea centrale. Il piano di campionamento deve definire quale geometria viene controllata, which secondary characteristics are checked, dove il contatto è consentito e quando è richiesto un processo indipendente.
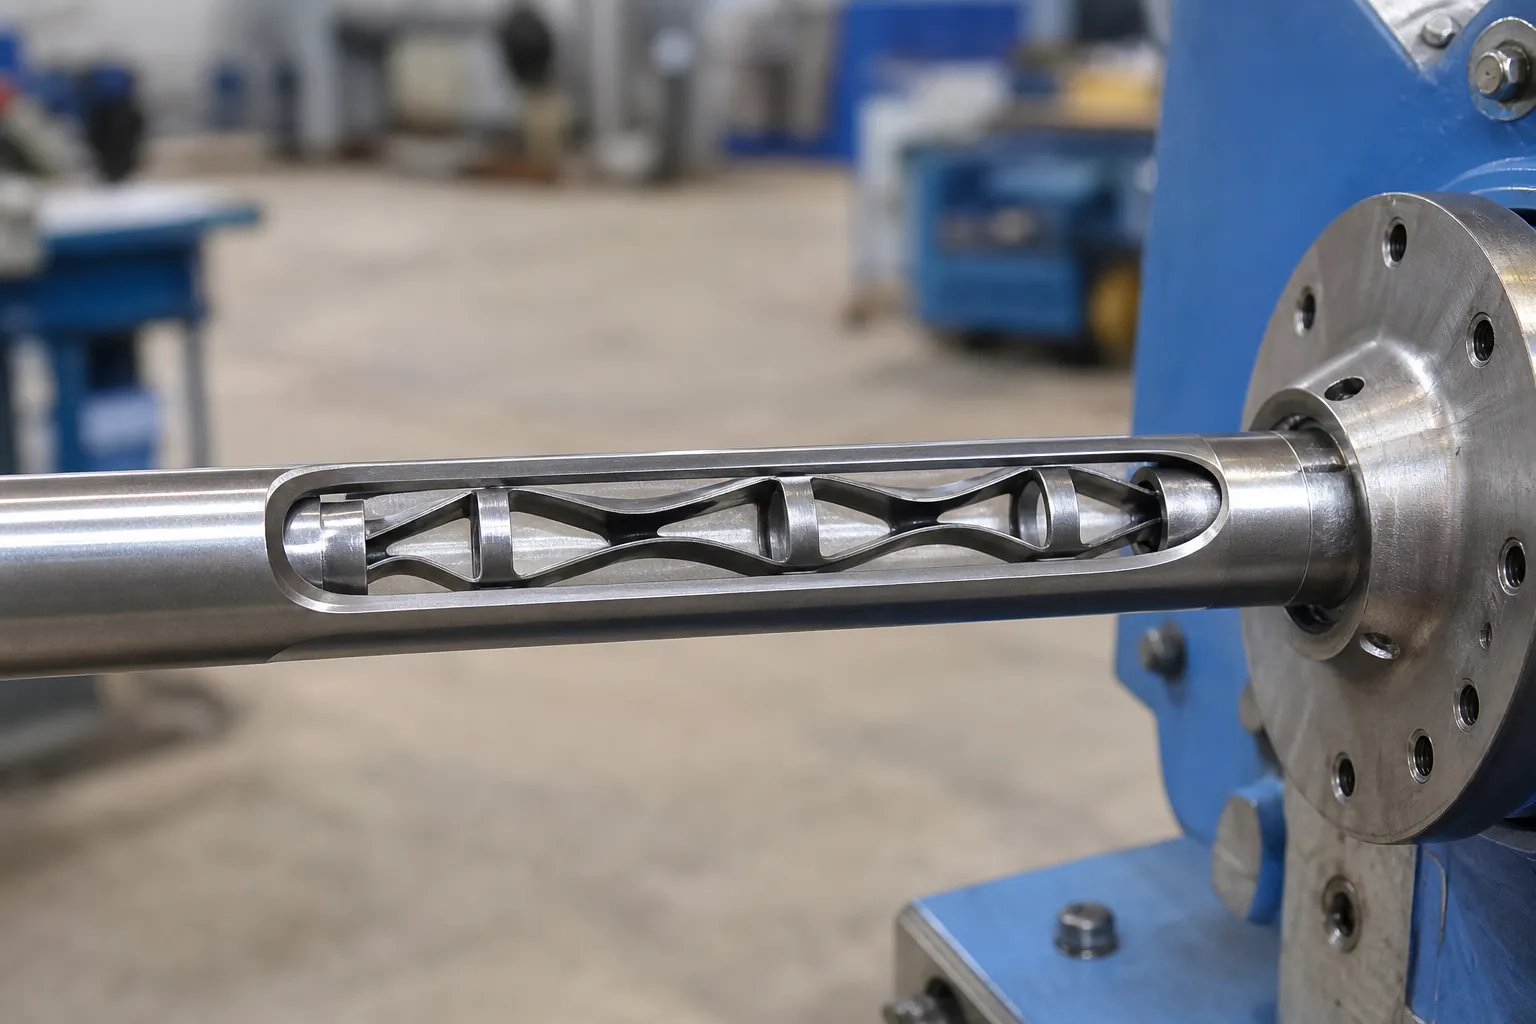
*Illustrazione del concetto di ingegneria. Presenta il supporto interno come una domanda di ingegneria del candidato; non si intende affermare che l'attrezzatura interna sia standard o appropriata per ogni tubo.*
For non-round hollow sections, see square and rectangular tube straightening. For hollow rotating parts, Vedere raddrizzatura di alberi cavi a pareti sottili.
Separate the Two Signals Before Accepting Either Reading
The two characteristics contaminate each other's measurements in specific, diagnosable ways. In a rotating single-probe trace at one station, the radial signal contains at least the local form error of the section and the offset of the section center from the rotation axis. Ovality-dominated form error appears primarily as a second harmonic — the trace repeats twice per revolution, with the ovality major axis setting the phase. A center offset appears as a first harmonic — one bump per revolution. Within a single trace the two are separable in principle, but the first harmonic itself is ambiguous: a genuine bend and a seating or chucking offset produce the same single-station signature. The discriminators live outside the single trace. Across stations, a bend changes amplitude with longitudinal position and follows the bend plane, while a seating offset keeps a constant amplitude and a phase locked to the rotation axis. That multi-station logic, together with the harmonic fingerprints of lobing and datum effects, is developed in rotondità vs piegatura nella misurazione rotante.
The contamination also runs the other way. A probe scanned along the tube reads the local surface, non l'asse: a tube that is straight on its centerline but drifting in ovality orientation along its length produces a lengthwise trace that looks like bow. A practical two-scan check costs little: scan the length in one direction, then in the orthogonal direction — by rotating the tube ninety degrees against the same probe, or by using a second probe at right angles. Compare the two traces. A centerline bow decomposes into the two directions as projections of one vector: the two traces are similar in shape and same in sign, each a scaled copy of the other. Section form does the opposite: where the ovality major axis lies in the first scan direction it lies across it in the second, so a peak in one trace corresponds to a valley in the other. Traces that are same-shape-same-sign nominate a bend; traces that are opposite-sign at particular stations nominate form and wall variation. Only the first category should go to a correction decision.
Wall-thickness eccentricity adds a third layer on drawn or rolled tube: the outside surface and the bore are not concentric, so a centerline computed from outside-diameter measurements and one computed from bore measurements will not coincide. Neither is wrong; they answer different functional questions. Which one governs acceptance must follow the function of the part in its assembly — and the drawing, not whichever gauge happens to be available, defines it. Thin-wall behavior during correction has its own failure modes, coperto Raddrizzamento di tubi a parete sottile senza collasso.
Build a Customer-Gauge Correlation Plan
The trial should use representative normal and worst-case tubes, letture grezze per entrambe le caratteristiche, condizioni concordate di supporto e rilascio, ripetere la configurazione, controlli superfici/pareti, e confronto con l'indicatore del cliente. The record should state whether a reading is a machine process value, a customer acceptance value or a correlated result.
Utilizzo correlazione tra scartamento della macchina e scartamento del cliente E prova e accettazione del campione di raddrizzatura per definire il pacchetto di prove.
Run Two Separate Acceptance Chains, Not One
Because the definitions, supports and failure modes differ, ovality and centerline straightness each need their own chain from drawing language to signed record. Collapsing both into one generic “geometry OK” leaves every link below ambiguous:
| Chain link | Ovality chain | Centerline chain |
|---|---|---|
| Characteristic and formula | Which deviation rule, applied per station | Which span governs, and which center-finding rule feeds the path |
| Metodo di riferimento | Section measurement at defined stations | Lengthwise scan or rotating trace on defined supports |
| Support and release | Free stations distinguished from supported stations | Span defined; sag and clamping effects addressed or correlated |
| Sampling | Station positions fixed by the specification, non per comodità | Station spacing short enough to resolve the shortest expected bend |
| Capacità di calibro | Repeatability proven against within-part form variation | Repeatability proven against part-to-part and setup variation |
| Correlazione | Machine gauge vs customer gauge on the same sections | Machine gauge vs customer gauge on the same span and supports |
| Documentazione | Per-station values with rule and station identity | Path result with support span and filtering stated |
Each link is a place the chain silently breaks. An unstated formula makes two gauges' numbers incomparable. A support condition defined at the machine but not at the customer builds a systematic offset into every correlation attempt. An unspecified station set makes the verdict depend on where the operator happened to measure. And an unproven gauge capability converts measurement noise into apparent process drift, which the correction loop then chases. Validating the measurement system before trusting any of these numbers is covered in calibro R&R per raddrizzare le linee.
Domande frequenti
Può un tubo essere dritto ma non rotondo??
SÌ. Centerline straightness and ovality are different conditions and require separate measurement. In practice the two belong in the same inspection record but under different characteristic numbers, each with its own formula, station set and gauge correlation.
Does a round cross-section prove the tube is straight over its length?
NO. A tube may be round at measured sections while its centerline has bow or sweep. A lengthwise scan reads the surface rather than the axis, so the orthogonal two-scan comparison above is what keeps form effects out of the straightness verdict.
Può un processo di correzione garantire entrambi i risultati??
Non senza una validazione specifica del pezzo. The process must measure and verify every characteristic required by the drawing. In particular, a process validated for bow says nothing about its effect on section form at contacts, supports and free stations — those need their own before-and-after readings.
How can we tell whether a straightness reading is contaminated by ovality?
Repeat the lengthwise scan in the orthogonal direction and compare the traces. Same shape and same sign across the two scans is the signature of a centerline bow; opposite sign at particular stations points to section form or wall variation. Rotating single-station traces add a second test: a bend changes amplitude between stations, while a seating offset does not.
Does ovality need to be measured at every cross-section?
Only the specification can answer that. What the acceptance plan must guarantee is that the station set is fixed in advance — typically including supports, morsetti, ends and the neighborhoods of bend peaks — so the verdict does not depend on where an operator happened to check.
*Illustrazione del concetto di ingegneria.*