
La protezione della superficie durante la stiratura è una decisione ingegneristica, non semplicemente aggiungendo un cuscinetto morbido. Il materiale del pezzo, sezione, fine, rivestimento, lubrificazione, geometria del contatto, percorso di forza, la pulizia degli utensili e le condizioni di usura possono influenzare i segni, appiattimento, danno locale e il segnale geometrico utilizzato per controllare il processo. Un metodo di contatto accettabile per una barra, il filo o l'albero potrebbero non essere accettabili per un tubo rivestito, giornale di precisione, angolo del profilo o utensile finito.
Questa guida spiega un framework di convalida. Non afferma che StraighteningTech abbia un particolare materiale in rotolo, rivestimento, forma della scanalatura, limite di pressione o capacità della superficie del pezzo. Tali elementi richiedono prove provenienti da strumenti reali e campioni rappresentativi.
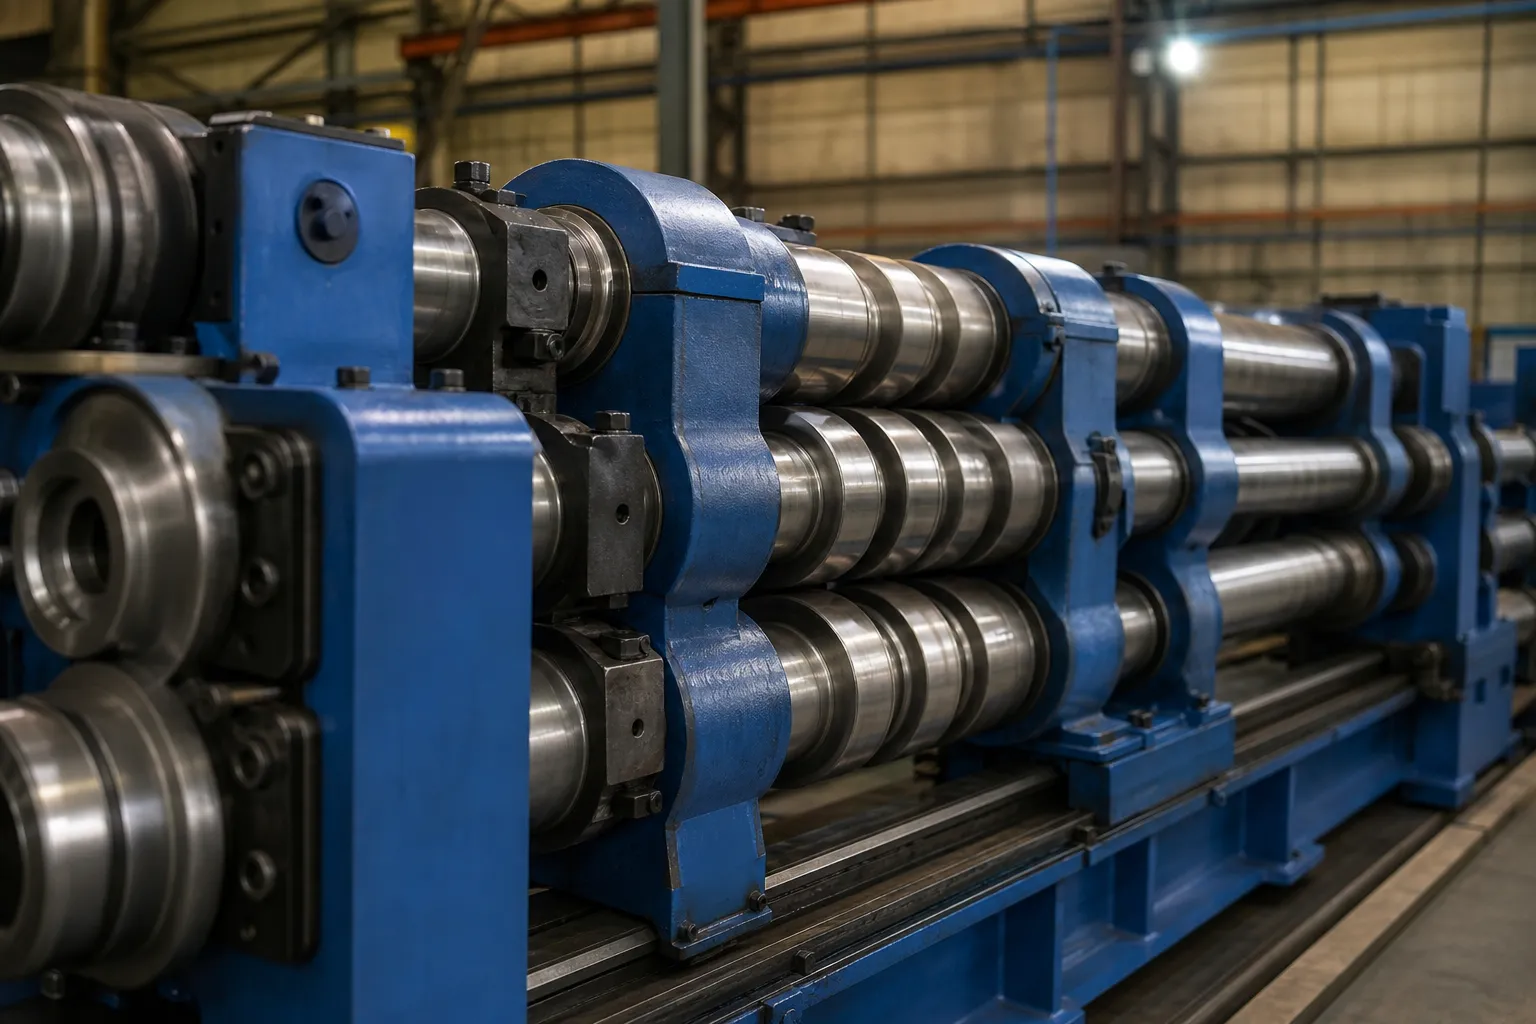
*Illustrazione del concetto di ingegneria. Mostra la protezione del rivestimento come un problema di validazione specifico del pezzo, nessuna prova di una scanalatura universale o di un materiale di contatto approvato.*
Prima di un processo, documentare l'identità dello strumento, materiale/finitura dove noto, geometria del contatto, posizione di installazione, allineamento, metodo di pulizia, condizioni di lubrificazione, ove applicabile, standard di ispezione e soglia di sostituzione/usura.
Where Marks Actually Come From
Surface damage in straightening has a short list of physical causes, and naming them is the first step to controlling them. Normal contact pressure between tooling and workpiece, multiplied by any relative sliding, produces the classic witness line. Debris trapped in the contact zone — scale, patatine, grinding swarf — converts ordinary pressure into indentation and scratching, which is why cleanliness is a process variable rather than housekeeping. A contact geometry that concentrates load on an edge or a radius that is too small for the section raises local stress far above what the average force suggests. And beyond a threshold specific to each material and heat-treatment state, local plastic flattening of asperities or of the section itself changes surface geometry permanently. A bruised corner on a profile or a flattened zone on a thin wall is a geometry defect, not only a cosmetic one.
Every one of those causes has a countermeasure that lives in tooling design and process discipline: distribute force through larger or conforming contact areas, eliminate sliding by aligning the correction stroke with the support plane, exclude debris through scheduled cleaning and covers, and keep forces within the range the section can carry elastically. None of them is a pad. Soft inserts are one option among several, and they bring their own trade-offs — softer contact materials wear faster, deform under sustained correction cycles, and can change the effective support geometry as they age, which quietly alters the correction result.
Tooling Material and Contact Geometry Decisions
Selecting contact tooling is a three-way trade between surface protection, dimensional stability of the tooling itself, and wear life. Hardened steel tooling holds its groove geometry through long runs and keeps the measurement-and-correction loop repeatable, but it concentrates contact stress and tolerates no debris. Softer non-ferrous alloys and polymer inserts lower local stress and forgive small particles, at the cost of faster wear and periodic requalification of the contact form. Conformal contact — a groove or saddle matched to the section radius — spreads load compared with a flat anvil face, and generous radii on every edge that can touch the workpiece remove the stress concentrations that cause bruising even at moderate force.
Two disciplines make those choices verifiable instead of habitual. Primo, each tooling element needs an identity: materiale, contact form, the workpiece zones it is approved for, and a wear limit stated as a measurable criterion — profile deviation of the groove, visible embedding, dimensional change of the insert — not as a judgment call. Secondo, a change in any contact component is a process change: the first parts after a roll change, an insert renewal or a re-ground anvil run under the same sample-test evidence rules as a new setup, because the surface and geometry result must be reconfirmed, non scontato. These are the same change-control habits that machine FAT checklists enforce at acceptance, applied daily.
Mantenere gli strumenti puliti e controllare l'usura
Detriti incorporati, scanalature usurate, rulli danneggiati, il disallineamento e la regolazione incoerente possono produrre segni o geometrie fuorvianti. Un piano di protezione dovrebbe specificare la frequenza delle ispezioni, metodo di pulizia, criteri di usura, controllo del cambio utensile e controllo di riqualificazione dopo la modifica di un componente di contatto. Non dovrebbe fare affidamento su una dichiarazione visiva secondo cui gli strumenti "sembrano a posto".
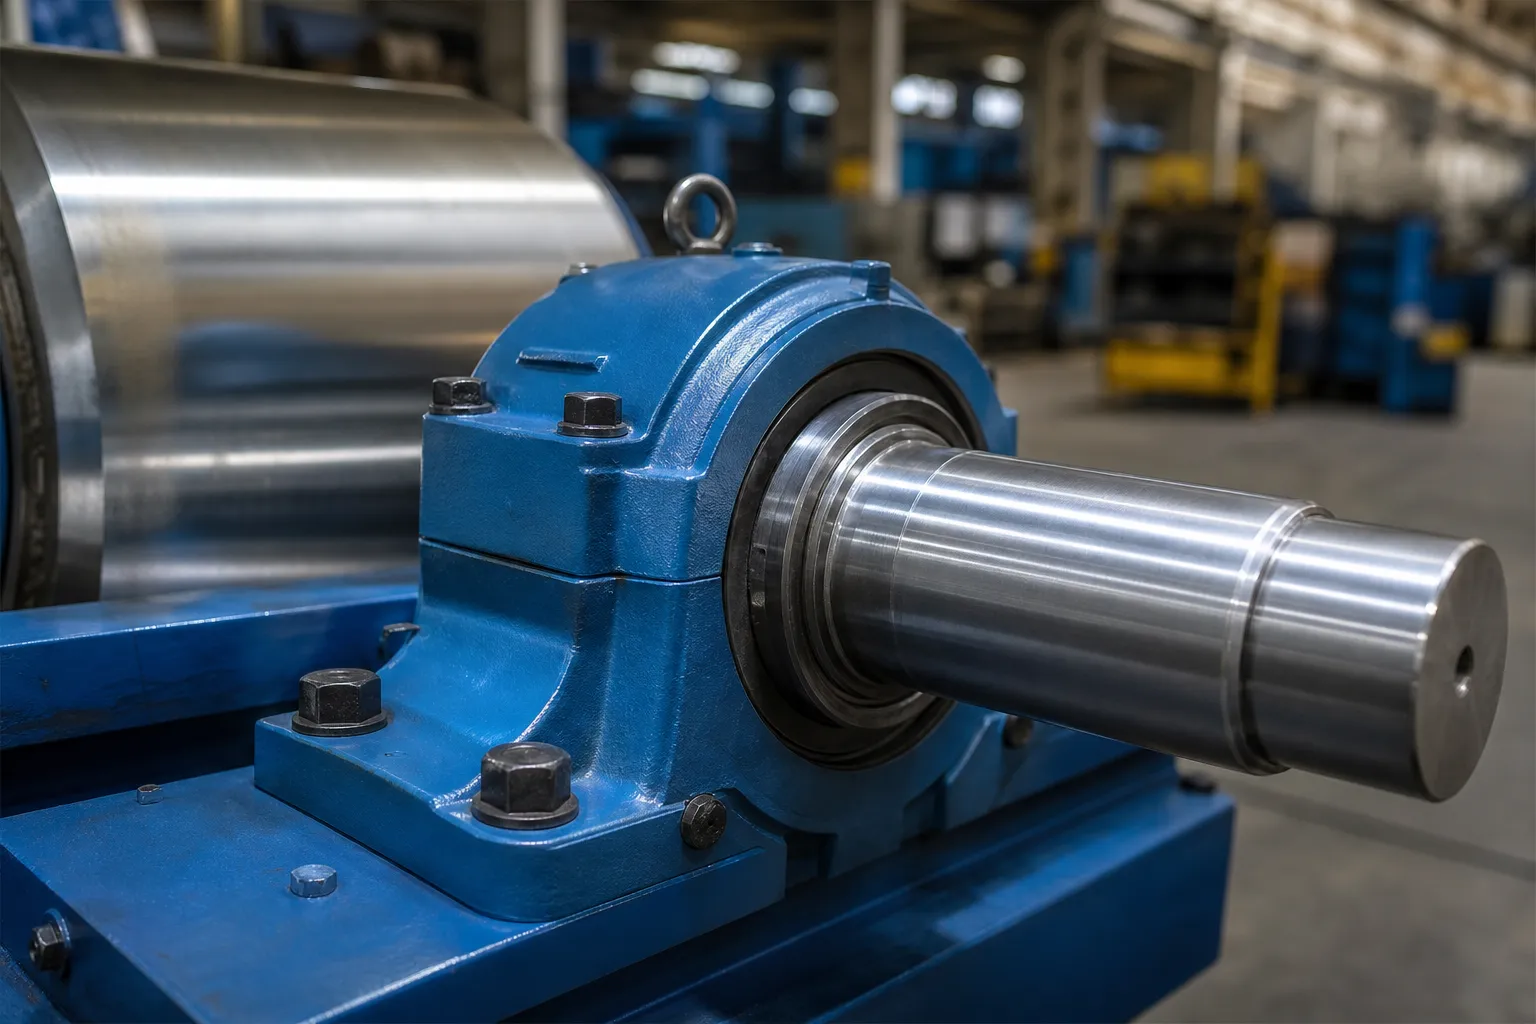
*Illustrazione del concetto di ingegneria. Descrive il contatto protetto come un requisito tecnico; non stabilisce un materiale del rullo locale, limite di pressione o garanzia della qualità della superficie.*
Convalida insieme superficie e geometria
La protezione della superficie non può essere convalidata solo controllando la presenza di graffi visibili. Il test del campione deve inoltre confermare la geometria prevista con il riferimento approvato e lo stato rilasciato. Un percorso che protegge la superficie ma non riesce a soddisfare la geometria richiesta non è accettabile; un percorso che rispetta la geometria ma danneggia un rivestimento funzionale non è accettabile.
| Elemento di convalida | Prove richieste |
|---|---|
| Posizione del contatto e percorso di reazione | Record di attrezzature/attrezzature collegate alle zone di disegno |
| Condizioni superficiali | Metodo di ispezione concordato prima e dopo la correzione |
| Risultato della geometria | Letture dello stato rilasciato sul dato/indicatore approvato |
| Ripetibilità degli utensili | Ripeti la configurazione, controllo pulizia e usura |
| Cambia controllo | Identificazione e rivalidazione dopo cambio rullo/scanalatura/utensile |
Utilizzo prova e accettazione del campione di raddrizzatura per definire il pacchetto di prove, E pressa rispetto alla raddrizzatura a rullo per determinare se debba essere valutato un diverso metodo di correzione.
The Force Path Matters More Than the Pad
The most common surface-protection failure is treating contact risk as a material question while ignoring load path. Where the supports sit, where the press point acts, and how those locations relate to the stiff features of the section determine how much force the operation needs in the first place. A correction stroke applied mid-span between widely spaced supports demands far more force — and leaves far deeper witness marks — than the same correction applied with supports closer to the correction point, even with identical tooling. Aligning the press axis with the support plane so the part does not slide or rotate under load removes the sliding component of damage entirely. On sections with asymmetric stiffness, pressing in the wrong direction loads a thin wall in bending and creates local dents that no insert material can prevent.
This is why surface protection is designed jointly with the correction plan, not bolted on afterward. The error map that drives the correction points should also mark the zones where contact is forbidden — finished journals, coating on sealing surfaces, polished flanks — and the tooling layout should place supports and press points where the section can carry the load. When those two requirements conflict, that is precisely the signal to escalate to the alternative routes discussed below, following the disposition logic used when NOK parts are sorted and reworked.
Surface Classes and Their Sensitivity
Not all surfaces need the same level of protection, and treating them identically either wastes effort or ruins parts. The table below groups workpiece surfaces by their sensitivity drivers and the validation focus each class demands. It is a planning aid for the sample test, not a substitute for drawing requirements.
| Surface class | Sensitivity driver | Validation focus |
|---|---|---|
| Ground or turned journals | Dimensional and form tolerance on functional diameters | Witness depth against tolerance; geometry re-check at the journal |
| Plated or coated surfaces | Coating integrity; cracking or adhesion under local stress | Agreed coating inspection before and after correction |
| Polished flanks and edges | Cosmetic and functional roughness levels | Defined finish comparison method, not unaided visual judgment |
| Soft non-ferrous sections | Low hardness; risk of permanent flattening | Contact-area limits; section form re-measurement |
| Thin-wall sections | Local denting and ovalization from concentrated load | Support placement under stiff zones; roundness checks after correction |
| Functional edges on tools | Cutting geometry and edge preparation | Edge condition inspection; correction only in non-functional zones |
Cutting-tool shanks and flutes are the extreme case of the last row, which is why raddrizzatura di punte a pistola e punte per fori profondi treats contact-zone protection as a first-order process input alongside datum selection. The same hierarchy — classify the surface, define the inspection, prove the route on samples — scales down to ordinary bar work.
Quando il rischio superficiale richiede un percorso diverso
Se le zone di contatto disponibili non possono preservare l'integrità della superficie o della sezione richiesta, la decisione corretta potrebbe essere uno strumento diverso, una fase di lavorazione diversa, un diverso metodo di correzione, indennità aggiuntiva, una strategia di misurazione senza contatto, o una revisione tecnica ATTESA in attesa. Non forzare una parte attraverso un percorso non convalidato per soddisfare un obiettivo di produzione. Saldato liquid cooling manifolds are one workpiece family where contact-zone risk must be reviewed before any press cycle.
Per confini di pareti sottili e rivestimenti, Vedere raddrizzatura di alberi cavi a pareti sottili E misurazione della rettilineità a contatto rispetto a quella senza contatto.
Domande frequenti
I cuscinetti morbidi prevengono tutti i danni alla superficie?
NO. Geometria del contatto, percorso di forza, detriti, Indossare, l'allineamento e la superficie del pezzo necessitano tutti di convalida.
È possibile riutilizzare una scanalatura per rullatura per ogni sezione?
NO. Geometria della sezione, condizione della parete, i requisiti di superficie e il percorso di reazione determinano se una scanalatura è adatta.
La sola ispezione visiva è sufficiente??
NO. Il processo deve inoltre dimostrare la geometria dello stato rilasciato e il metodo di accettazione della superficie/caratteristica concordato.
Which surface classes need protection most?
Plated or coated surfaces, polished flanks, soft non-ferrous sections, thin walls and functional edges on cutting tools. Each class has a different failure mode — coating cracking, appiattimento, ammaccatura, edge damage — so the inspection method has to match the failure mode, and the sample test must prove both surface and released-state geometry.
How is tooling wear turned into an objective criterion?
By writing a measurable limit into the tooling record before production starts: groove profile deviation from the original form, dimensional change of inserts, embedded debris that cleaning cannot remove, or a counted number of correction cycles. When the limit is reached, the tooling element is replaced or reconditioned and the first parts after the change are requalified under sample-test rules.
Does support placement really affect surface damage?
SÌ, strongly. Support span and press-point location determine the force the operation needs, and edge radii determine how that force concentrates. Moving supports closer to the correction zone and keeping every contact edge radiused often reduces witness severity more than any change of insert material, because it attacks force and geometry instead of only the contact pair.
*Illustrazione del concetto di ingegneria.*
Stiratura prima o dopo la placcatura o il rivestimento
Stiratura prima o dopo la placcatura o il rivestimento viene gestito come un argomento relativo al contatto superficiale e al rischio degli strumenti piuttosto che come un URL autonomo. Esaminare la durezza del rivestimento, contattare i limiti di sollecitazione e rilavorazione sulla pagina degli utensili di protezione superficiale e sulla pagina del relativo pezzo prima di scegliere la fase di raddrizzatura.
Surface protection decisions like these show up directly on the finished part – IL guida ai segni degli utensili covers contact damage in detail, E stiramento eccessivo e screpolature covers the deformation side of the same risk.