
Surface protection in straightening is an engineering decision, not simply adding a soft pad. The workpiece material, سیکشن, ختم, کوٹنگ, چکنا, رابطہ جیومیٹری, طاقت کا راستہ, tooling cleanliness and wear condition can each influence marks, flattening, local damage and the geometry signal used to control the process. A contact method that is acceptable for one bar, wire or shaft may be unacceptable for a coated tube, precision journal, profile corner or finished tool.
This guide explains a validation framework. It does not claim that StraighteningTech has a particular roll material, کوٹنگ, groove form, pressure limit or workpiece surface capability. Those items require evidence from the actual tooling and representative samples.
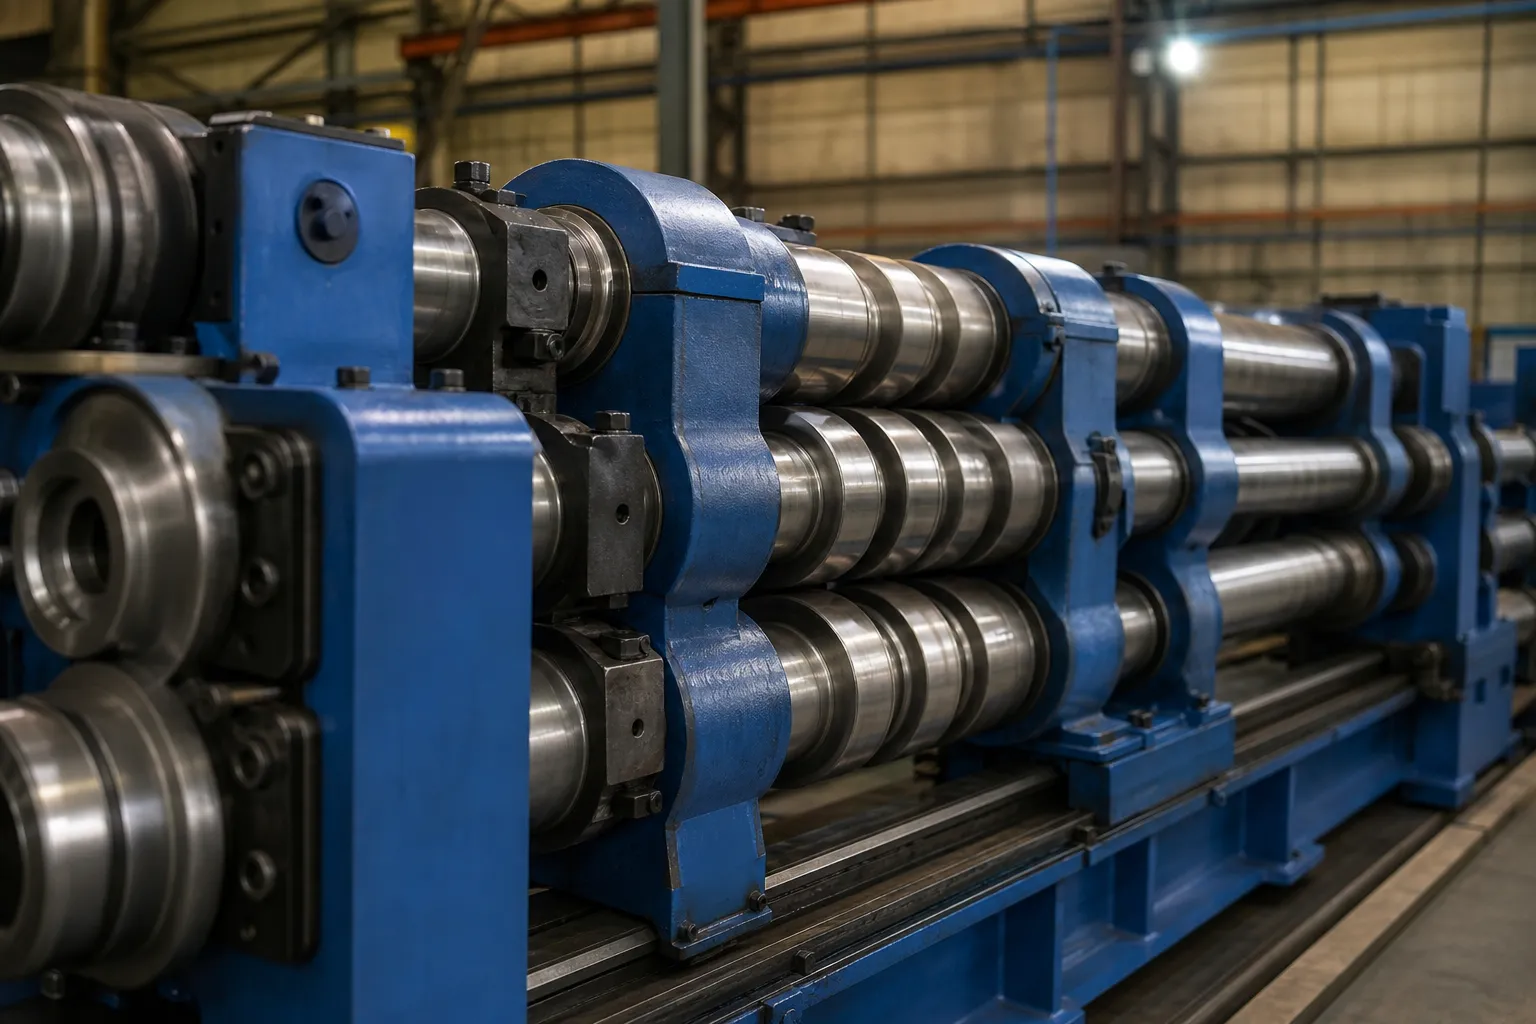
*انجینئرنگ تصور کی مثال. It shows coating protection as a workpiece-specific validation issue, منظور شدہ یونیورسل گروو یا رابطہ مواد کا ثبوت نہیں ہے۔*
مقدمے کی سماعت سے پہلے, آلے کی شناخت کو دستاویز کریں۔, مواد/ختم جہاں جانا جاتا ہے۔, رابطہ جیومیٹری, سیٹ اپ مقام, سیدھ, صفائی کا طریقہ, پھسلن کی حالت جہاں قابل اطلاق ہو۔, معائنہ کا معیار اور تبدیلی/پہن کی حد.
Where Marks Actually Come From
Surface damage in straightening has a short list of physical causes, and naming them is the first step to controlling them. Normal contact pressure between tooling and workpiece, multiplied by any relative sliding, produces the classic witness line. Debris trapped in the contact zone — scale, chips, grinding swarf — converts ordinary pressure into indentation and scratching, which is why cleanliness is a process variable rather than housekeeping. A contact geometry that concentrates load on an edge or a radius that is too small for the section raises local stress far above what the average force suggests. And beyond a threshold specific to each material and heat-treatment state, local plastic flattening of asperities or of the section itself changes surface geometry permanently. A bruised corner on a profile or a flattened zone on a thin wall is a geometry defect, not only a cosmetic one.
Every one of those causes has a countermeasure that lives in tooling design and process discipline: distribute force through larger or conforming contact areas, eliminate sliding by aligning the correction stroke with the support plane, exclude debris through scheduled cleaning and covers, and keep forces within the range the section can carry elastically. None of them is a pad. Soft inserts are one option among several, and they bring their own trade-offs — softer contact materials wear faster, deform under sustained correction cycles, and can change the effective support geometry as they age, which quietly alters the correction result.
Tooling Material and Contact Geometry Decisions
رابطہ ٹولنگ کا انتخاب سطح کے تحفظ کے درمیان تین طرفہ تجارت ہے۔, خود ٹولنگ کی جہتی استحکام, اور زندگی پہن لو. سخت سٹیل ٹولنگ اس کی نالی جیومیٹری کو لمبی دوڑ میں رکھتی ہے اور پیمائش اور تصحیح لوپ کو دہرانے کے قابل رکھتی ہے۔, لیکن یہ رابطے کے تناؤ کو مرکوز کرتا ہے اور کوئی ملبہ برداشت نہیں کرتا ہے۔. نرم الوہ مرکبات اور پولیمر مقامی دباؤ کو کم کرتے ہیں اور چھوٹے ذرات کو معاف کرتے ہیں۔, تیزی سے پہننے کی قیمت پر اور رابطہ فارم کی متواتر قابلیت. رسمی رابطہ - سیکشن کے رداس سے مماثل ایک نالی یا سیڈل - فلیٹ اینول چہرے کے مقابلے میں بوجھ پھیلاتا ہے, اور ہر کنارے پر فرحت بخش ریڈیائی جو ورک پیس کو چھو سکتی ہے تناؤ کے ارتکاز کو دور کرتی ہے جو اعتدال پسند قوت پر بھی چوٹ کا باعث بنتی ہے۔.
Two disciplines make those choices verifiable instead of habitual. سب سے پہلے, each tooling element needs an identity: مواد, contact form, the workpiece zones it is approved for, and a wear limit stated as a measurable criterion — profile deviation of the groove, visible embedding, dimensional change of the insert — not as a judgment call. دوسرا, a change in any contact component is a process change: the first parts after a roll change, an insert renewal or a re-ground anvil run under the same sample-test evidence rules as a new setup, because the surface and geometry result must be reconfirmed, فرض نہیں کیا. These are the same change-control habits that مشین FAT چیک لسٹ enforce at acceptance, applied daily.
ٹولنگ کو صاف رکھیں اور پہننے کو کنٹرول کریں۔
سرایت شدہ ملبہ, پہنے ہوئے نالیوں, خراب رولر, غلط ترتیب اور متضاد ایڈجسٹمنٹ نشانات یا گمراہ کن جیومیٹری پیدا کر سکتی ہے۔. ایک حفاظتی منصوبہ معائنہ کی تعدد کی وضاحت کرے۔, صفائی کا طریقہ, پہننے کے معیار, تبدیل شدہ رابطہ جزو کے بعد ٹول کی تبدیلی کا کنٹرول اور دوبارہ قابلیت کی جانچ. اسے کسی بصری بیان پر انحصار نہیں کرنا چاہئے کہ ٹولنگ "ٹھیک نظر آتی ہے۔"
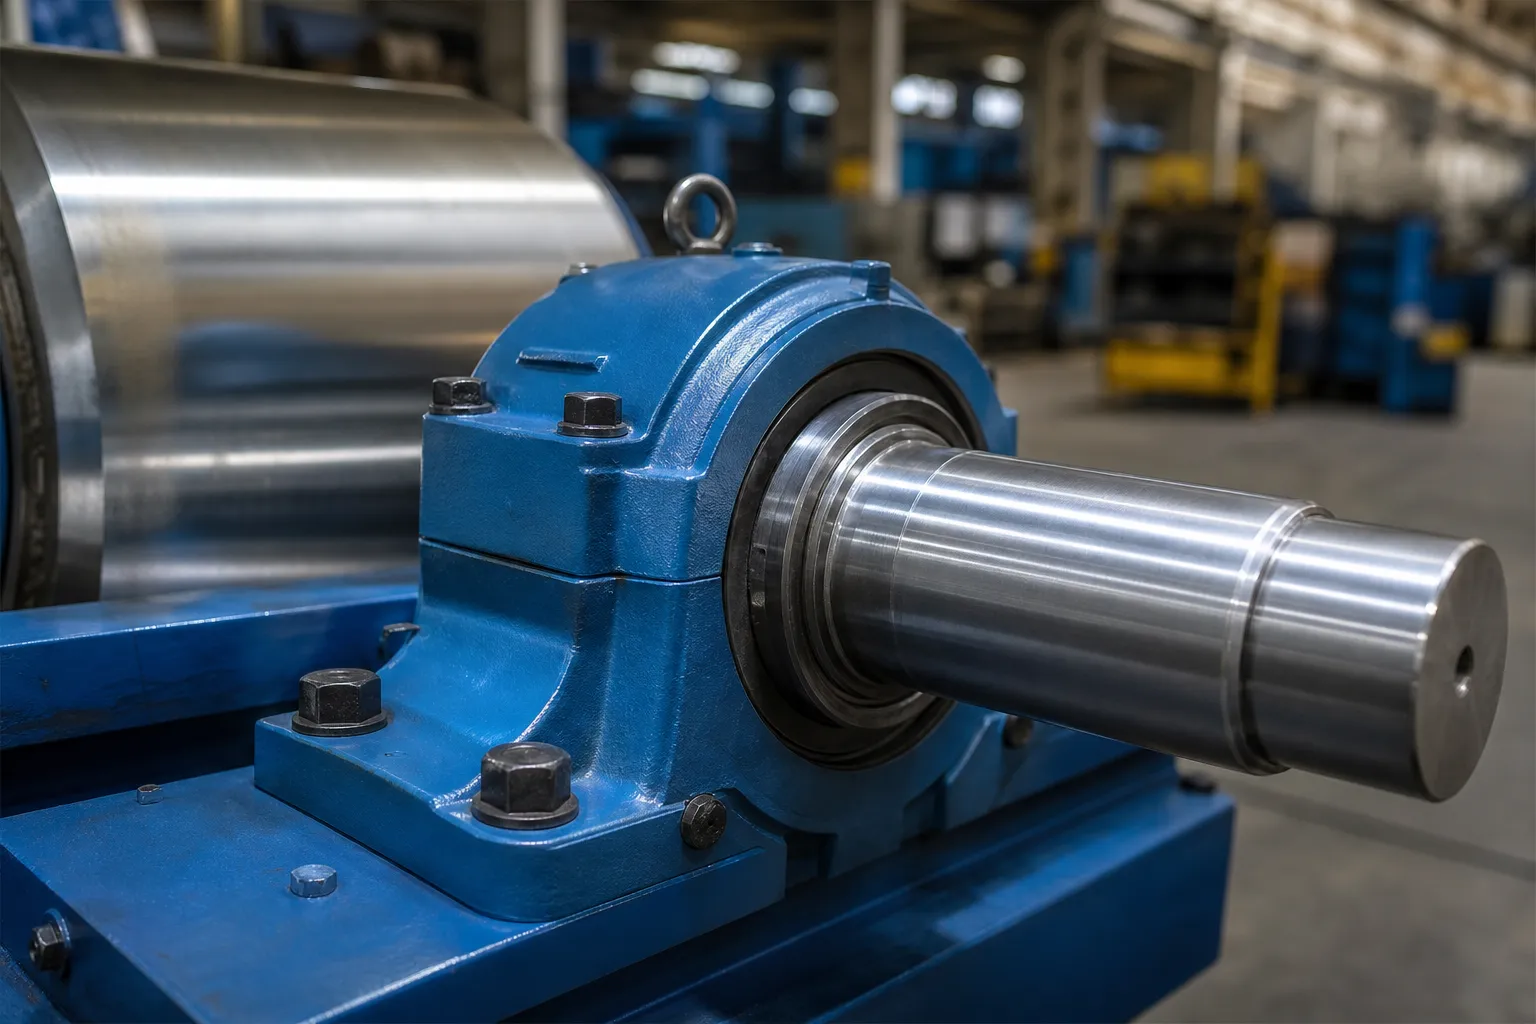
*انجینئرنگ تصور کی مثال. یہ انجینئرنگ کی ضرورت کے طور پر محفوظ رابطے کو ظاہر کرتا ہے۔; یہ مقامی رولر مواد قائم نہیں کرتا ہے۔, pressure limit or surface-quality guarantee.*
Validate Surface and Geometry Together
Surface protection cannot be validated only by checking for visible scratches. The sample test must also confirm the intended geometry under the approved datum and released state. A route that protects the surface but cannot meet the required geometry is not acceptable; a route that meets geometry but damages a functional coating is not acceptable.
| Validation item | ثبوت درکار ہے۔ |
|---|---|
| Contact location and reaction path | Tooling/setup record linked to drawing zones |
| سطح کی حالت | Agreed inspection method before and after correction |
| جیومیٹری کا نتیجہ | Released-state readings on the approved datum/gauge |
| Tooling repeatability | Repeat setup, cleanliness and wear check |
| Change control | Identification and revalidation after roll/groove/tool change |
استعمال کریں۔ سیدھا نمونہ ٹیسٹ اور قبولیت to define the evidence pack, اور رولر سیدھا کرنے کے مقابلے میں دبائیں اس بات کا تعین کرنے کے لیے کہ آیا ایک مختلف تصحیح کے طریقہ کار کا جائزہ لیا جانا چاہیے۔.
The Force Path Matters More Than the Pad
سطح کے تحفظ میں سب سے عام ناکامی رابطے کے خطرے کو ایک مادی سوال کے طور پر سمجھنا ہے جبکہ بوجھ کے راستے کو نظر انداز کیا جاتا ہے۔. جہاں حمایتی بیٹھتے ہیں۔, جہاں پریس پوائنٹ کام کرتا ہے۔, اور وہ مقامات کس طرح سیکشن کی سخت خصوصیات سے متعلق ہیں اس بات کا تعین کرتے ہیں کہ آپریشن کو پہلی جگہ کتنی طاقت کی ضرورت ہے۔. وسیع پیمانے پر فاصلہ رکھنے والے سپورٹ کے درمیان وسط مدت میں لاگو کیا گیا ایک اصلاحی اسٹروک بہت زیادہ طاقت کا مطالبہ کرتا ہے — اور بہت زیادہ گہرے گواہی کے نشان چھوڑتا ہے — اس کے مقابلے میں وہی اصلاح جو تصحیح کے نقطہ کے قریب سپورٹ کے ساتھ لاگو ہوتی ہے۔, ایک جیسی ٹولنگ کے ساتھ بھی. پریس محور کو سپورٹ ہوائی جہاز کے ساتھ سیدھ میں کرنا تاکہ حصہ سلائیڈ نہ ہو یا بوجھ کے نیچے نہ گھومے نقصان کے سلائیڈنگ جزو کو مکمل طور پر ہٹا دیتا ہے۔. غیر متناسب سختی والے حصوں پر, pressing in the wrong direction loads a thin wall in bending and creates local dents that no insert material can prevent.
This is why surface protection is designed jointly with the correction plan, not bolted on afterward. The error map that drives the correction points should also mark the zones where contact is forbidden — finished journals, coating on sealing surfaces, polished flanks — and the tooling layout should place supports and press points where the section can carry the load. When those two requirements conflict, that is precisely the signal to escalate to the alternative routes discussed below, following the disposition logic used when NOK parts are sorted and reworked.
Surface Classes and Their Sensitivity
Not all surfaces need the same level of protection, and treating them identically either wastes effort or ruins parts. The table below groups workpiece surfaces by their sensitivity drivers and the validation focus each class demands. It is a planning aid for the sample test, not a substitute for drawing requirements.
| Surface class | Sensitivity driver | Validation focus |
|---|---|---|
| Ground or turned journals | Dimensional and form tolerance on functional diameters | Witness depth against tolerance; geometry re-check at the journal |
| Plated or coated surfaces | Coating integrity; cracking or adhesion under local stress | Agreed coating inspection before and after correction |
| Polished flanks and edges | Cosmetic and functional roughness levels | Defined finish comparison method, not unaided visual judgment |
| Soft non-ferrous sections | Low hardness; risk of permanent flattening | Contact-area limits; section form re-measurement |
| Thin-wall sections | Local denting and ovalization from concentrated load | Support placement under stiff zones; roundness checks after correction |
| Functional edges on tools | Cutting geometry and edge preparation | Edge condition inspection; correction only in non-functional zones |
Cutting-tool shanks and flutes are the extreme case of the last row, which is why گن ڈرل اور گہرے سوراخ کی ڈرل سیدھی کرنا treats contact-zone protection as a first-order process input alongside datum selection. The same hierarchy — classify the surface, define the inspection, prove the route on samples — scales down to ordinary bar work.
جب سطح کے خطرے کو مختلف راستے کی ضرورت ہوتی ہے۔
اگر دستیاب رابطہ زون مطلوبہ سطح یا حصے کی سالمیت کو محفوظ نہیں رکھ سکتے ہیں۔, صحیح فیصلہ ایک مختلف ٹول ہو سکتا ہے۔, ایک مختلف مینوفیکچرنگ کا مرحلہ, ایک مختلف اصلاح کا طریقہ, اضافی الاؤنس, غیر رابطہ پیمائش کی حکمت عملی, یا HOLD زیر التواء انجینئرنگ جائزہ. پیداواری ہدف کو پورا کرنے کے لیے کسی حصے کو غیر تصدیق شدہ راستے سے مجبور نہ کریں۔. ویلڈڈ liquid cooling manifolds are one workpiece family where contact-zone risk must be reviewed before any press cycle.
پتلی دیوار اور کوٹنگ کی حدود کے لیے, دیکھیں پتلی دیوار کے کھوکھلی شافٹ کو سیدھا کرنا اور رابطہ بمقابلہ غیر رابطہ سیدھے پن کی پیمائش.
اکثر پوچھے گئے سوالات
کیا نرم پیڈ تمام سطح کے نقصان کو روکنے کے?
نہیں. جیومیٹری سے رابطہ کریں۔, طاقت کا راستہ, ملبہ, پہننا, سیدھ اور ورک پیس کی سطح سبھی کو توثیق کی ضرورت ہے۔.
کیا رول گروو کو ہر سیکشن کے لیے دوبارہ استعمال کیا جا سکتا ہے؟?
نہیں. سیکشن جیومیٹری, دیوار کی حالت, سطح کی ضرورت اور رد عمل کا راستہ اس بات کا تعین کرتا ہے کہ آیا نالی موزوں ہے یا نہیں۔.
کیا صرف بصری معائنہ ہی کافی ہے۔?
نہیں. اس عمل کو جاری شدہ ریاست جیومیٹری اور سطح/فیچر قبول کرنے کا متفقہ طریقہ بھی ظاہر کرنا چاہیے۔.
Which surface classes need protection most?
Plated or coated surfaces, polished flanks, soft non-ferrous sections, thin walls and functional edges on cutting tools. Each class has a different failure mode — coating cracking, flattening, ڈینٹنگ, edge damage — so the inspection method has to match the failure mode, and the sample test must prove both surface and released-state geometry.
How is tooling wear turned into an objective criterion?
By writing a measurable limit into the tooling record before production starts: groove profile deviation from the original form, dimensional change of inserts, embedded debris that cleaning cannot remove, or a counted number of correction cycles. When the limit is reached, the tooling element is replaced or reconditioned and the first parts after the change are requalified under sample-test rules.
Does support placement really affect surface damage?
جی ہاں, strongly. Support span and press-point location determine the force the operation needs, and edge radii determine how that force concentrates. Moving supports closer to the correction zone and keeping every contact edge radiused often reduces witness severity more than any change of insert material, because it attacks force and geometry instead of only the contact pair.
*انجینئرنگ تصور کی مثال۔*
چڑھانا یا کوٹنگ کے بعد بمقابلہ پہلے سیدھا کرنا
چڑھانا یا کوٹنگ کے بعد بمقابلہ پہلے سیدھا کرنا اسٹینڈ اسٹون یو آر ایل کے بجائے سطحی رابطہ اور ٹولنگ کے خطرے والے موضوع کے طور پر ہینڈل کیا جاتا ہے۔. کوٹنگ کی سختی کا جائزہ لیں۔, سیدھا کرنے کے مرحلے کا انتخاب کرنے سے پہلے سطح کے تحفظ کے ٹولنگ پیج پر اور متعلقہ ورک پیس پیج پر تناؤ اور دوبارہ کام کی حدود سے رابطہ کریں۔.
Surface protection decisions like these show up directly on the finished part – دی ٹولنگ مارکس گائیڈ covers contact damage in detail, اور زیادہ سیدھا اور کریکنگ covers the deformation side of the same risk.