
Obsah
- Čo vlastne ohýba skrutky
- Short Bolt Straightening vs Long-Bolt Machines
- How to Make Good Bolt With Straightener Equipment: Korekčná slučka
- What a Bolt Straightening Machine Must Do for Short Parts
- The Short-Bolt Straightening Solution in Practice
- Bežné režimy porúch a ich prevencia
- FAQ
- Kde sa nachádza táto stránka
- References
Čo vlastne ohýba skrutky
Short bolts leave heat treatment bent more often than anyone likes, and the fix is not a hammer and a bench block. How to make good bolt with straightener equipment — dedicated press-straightening machinery — is a discipline of measured bends, controlled strokes, and verified acceptance. It also differs from long-bolt work in ways that matter to anyone specifying a machine, because a part with almost no span between its head and its thread punishes the wrong equipment choice.
Skreslenie skrutky je väčšinou príbehom o tepelnom spracovaní s manipulačným epilógom. Kalenie ochladzuje súčiastku nerovnomerne, zámky v stresoch, a časť sa ukloní, keď sa tieto stresy uvoľnia. The Precision Machined Products Association (PMPA) separates the two distortion modes plainly: dimensional change from phase transformation is expected and small, while warpage "is usually a result of process and design issues." Their heat-treat guidance lists eight recurring causes of warp on quench and temper — from rapid heating and non-uniform cooling to water contamination in the quench oil, large changes of mass and section, and asymmetric features — and explains the mechanism: "Non-uniform cooling allows unbalanced stresses to develop during the quench, as does non-uniform agitation of quench medium."
For sizing expectations, PMPA offers a working rule of thumb for medium carbon alloy steels: "a change in linear dimensions of about 0.125% maximum" from heat treatment and quench. That is the scale of the distortion budget before warpage even enters the picture. Thread rolling and machining add their own residual-stress history on top, which is why finished fasteners arrive at the straightening station with bends that no amount of careful handling will prevent.
Short bolts then add a twist of their own. Krátka skrutka je tuhšia ako dlhá s rovnakým priemerom, so it bends less from a given stress — but everything around it is tighter. The thread must gauge, the assembly must seat, and there is little room even for modest bows. The underlying mechanics of how prior deformation changes a part's response to correction — reverse loading and the Bauschingerov efekt — matter here as much as anywhere in straightening work.
Key takeaways
- Bolt bend is mainly a quench-distortion problem: non-uniform cooling and agitation leave unbalanced stresses that relax into a bow.
- Heat-treat dimensional change alone runs up to about 0.125% of linear dimensions on medium carbon alloy steels, per PMPA's rule of thumb.
- Short bolts are stiff but unforgiving: tighter effective tolerances and almost no span for correction make machine choice decisive.
Short Bolt Straightening vs Long-Bolt Machines
Je lákavé predstaviť si jeden univerzálny vyrovnávač skrutiek, ale fyzika tieto dve rodiny oddeľuje. Dlhý, štíhly svorník sa správa ako hriadeľ: ťaží zo skenovania po celej dĺžke, mapovanie krivky ohybu, and correcting at the mapped peaks — the approach behind our automatizované riešenie na vyrovnávanie skrutiek for the general automation case and the automatický proces vyrovnávania dlhých skrutiek. The research mechanics of that correction style are well established: Wang's over-bend straightening theory, published in the MDPI journal Metals v 2022, describes how "a zigzag straightening moment was applied in the three-point multi-step straightening process to approximate the smooth curve of theoretical moment" — in other words, long-part machines press at discrete mapped points, stepping along the length.
Watch the long-bolt machine family running at a customer site on YouTube: Zákaznícka stránka stroja na vyrovnávanie dlhých skrutiek — scan the length, zmapovať zákrutu, press at the mapped peaks, premerať. A short bolt offers almost no usable span between its head and thread, so the correction window is narrow from the start. Positioning accuracy of the part, precision of the press stroke, and protection of the thread zones dominate the result, while the bend map itself is simpler. Preto sa stroje s krátkym závitom sústreďujú na posuv, orientácia, precise localized correction, and fast gauging, kým systémy s dlhými skrutkami investujú do skenovania a viacbodovej stratégie.
Buyers specifying equipment should name which regime their parts live in. A machine optimized for one will process the other disappointingly — and for shaft-family parts beyond bolts, the same reasoning shapes our shaft straightening solutions.
How to Make Good Bolt With Straightener Equipment: Korekčná slučka
The process flow on any short-bolt line reads the same — zaťaženie, pozíciu, narovnať, test, discharge — but the engineering lives inside each step. The loop below is how the sequence earns its result.
Positioning Sets the Accuracy Budget
Umiestnenie je miesto, kde sa rozhoduje o väčšine presnosti. A bolt seated a fraction of a millimeter off its intended rotation axis reads as bent and gets corrected for a setup error, takže dátumové funkcie, seating cleanliness, and repeat-clamping behavior are the accuracy foundation of the whole line. Before a single press stroke, the fixture must present the same part, on the same datum, the same way, every cycle.
The Straightening Press Stroke
Narovnanie je najkratší krok a najmenej odpúšťa. The stroke is small, the response depends on the material's state, and the target follows from measured curvature: Wang's 2022 analysis builds the stroke on "the springback theory of small curvature plane bending," with the over-bend moment computed section by section. In the same paper's tube-straightening experiments, "the straightness of the straightened workpiece could be controlled within 1.5‰, which meets the standard requirements" — a research result on tubes, not a universal machine spec, but a measured anchor for what curvature-based stroke control achieves.
Over-correction on a short part is expensive because there is little span left for a counter-move. Each reverse press works the material again, and the accumulated load history changes how the next stroke behaves.
The Bauschinger Effect and the Cost of Over-Correction
Why does a part respond differently to its second press than its first? The Bauschinger effect. Witels Albert, a straightening-roll specialist, defines it in their Wire Straightening Glossary as "a change of material parameters due to a reversal of loading direction between two consecutive loads (napr. tension/compression)." Straightening is exactly such a reversal, which is why correction recipes cannot treat the second press like the first. The same glossary notes the magnitude depends on the material, its alloying elements (particularly carbon), "the number of load cycles, and the dimensions of external deformation (actual strains)" — two of the four factors sit under the process engineer's control, which is the entire argument for correction-attempt limits as policy. Our companion article on Bauschingerov efekt pri narovnávaní develops the mechanics.
Thread Protection During Automated Correction
Threads are the finished surface that pays for everyone else's mistakes. Protection is a contact-zone design problem: press and support contact belongs on the plain shank, tooling conforms to the section, edges are radiused everywhere a surface could touch, and feed routes keep bulk-fed parts from grinding each other. The proof is the inspection agreed before any trial — thread gauges and flank condition reviewed alongside the geometry result. The same discipline drives our nástroje na ochranu povrchu na vyrovnávanie practice.
Measuring and Accepting the Result
Straightness of finished bolts is not a matter of taste; it is standardized. ISO 4759-1 "specifies a selection of tolerances for bolts, skrutky, studs and nuts with ISO metric threads and with product grades A, B and C," and its product grades are ordered: "grade A is the most precise and grade C is the least precise." For shank straightness the standard gives tolerance formulas that scale with length — for shanks up to 8 priemer mm, t = 0.002 l + 0.05 mm; above 8 mm, t = 0.0025 l + 0.05 mm — so a 60 mm long M8 shank carries a straightness tolerance of about 0.17 mm by direct arithmetic. On the gaging side, ASME B18.2.9 "describes a gage and gaging procedure for checking bolt or screw straightness at maximum material condition (MMC)."
Two measurement disciplines protect the acceptance decision itself: meranie každej časti po korekcii, so zhodnými a nezhodnými časťami fyzicky oddelenými, podľa Rámec na triedenie a prepracovanie NOK — and defining the acceptance measure before gauging, because straightness, runout and TIR are not interchangeable terms; náš priamosť hriadeľa vs hádzanie vs TIR primer separates them. Parts measured in the fixture that fail free at the customer are an acceptance-rule failure, not a machine failure.
What a Bolt Straightening Machine Must Do for Short Parts
Machine capability for this part family is concrete, not adjectival. On our UBJ-80 bolt straightening machine — a go-through straightener built for heat-treated finished parts including screws and fasteners — "the range of bar lengths is from 60 do 600 mm, a rozsah priemerov je od φ3~φ25mm," with a machining speed of "3~5 sec/piece." Those are this machine family's published figures, verified per lot against the drawing's straightness definition, not free-floating promises.
Two further capabilities separate a short-part line from a long-part one. Po prvé, setup and adjustment burden: research on straightening-machine design (Bathelt et al., MDPI Sensors, 2023 — a flat-wire study) records that historically "the adjustment of a straightening machine has been performed manually, which is a lengthy and complex task even for an experienced worker," which is exactly the burden recipe management exists to remove on a high-mix short-part line. Po druhé, sensor information: the same paper's contribution — an integrated, precise straightening force measurement that makes feedback control practical — is the direction short-bolt machine design follows, because a part pressed in seconds gives the process no time for manual re-tuning.
Incoming condition is the machine's silent partner. Lots identified by heat-treatment state and grouped by bend severity feed a stable correction recipe; a line fed mixed lots spends its margin compensating for scatter that receiving inspection could have caught.
The Short-Bolt Straightening Solution in Practice
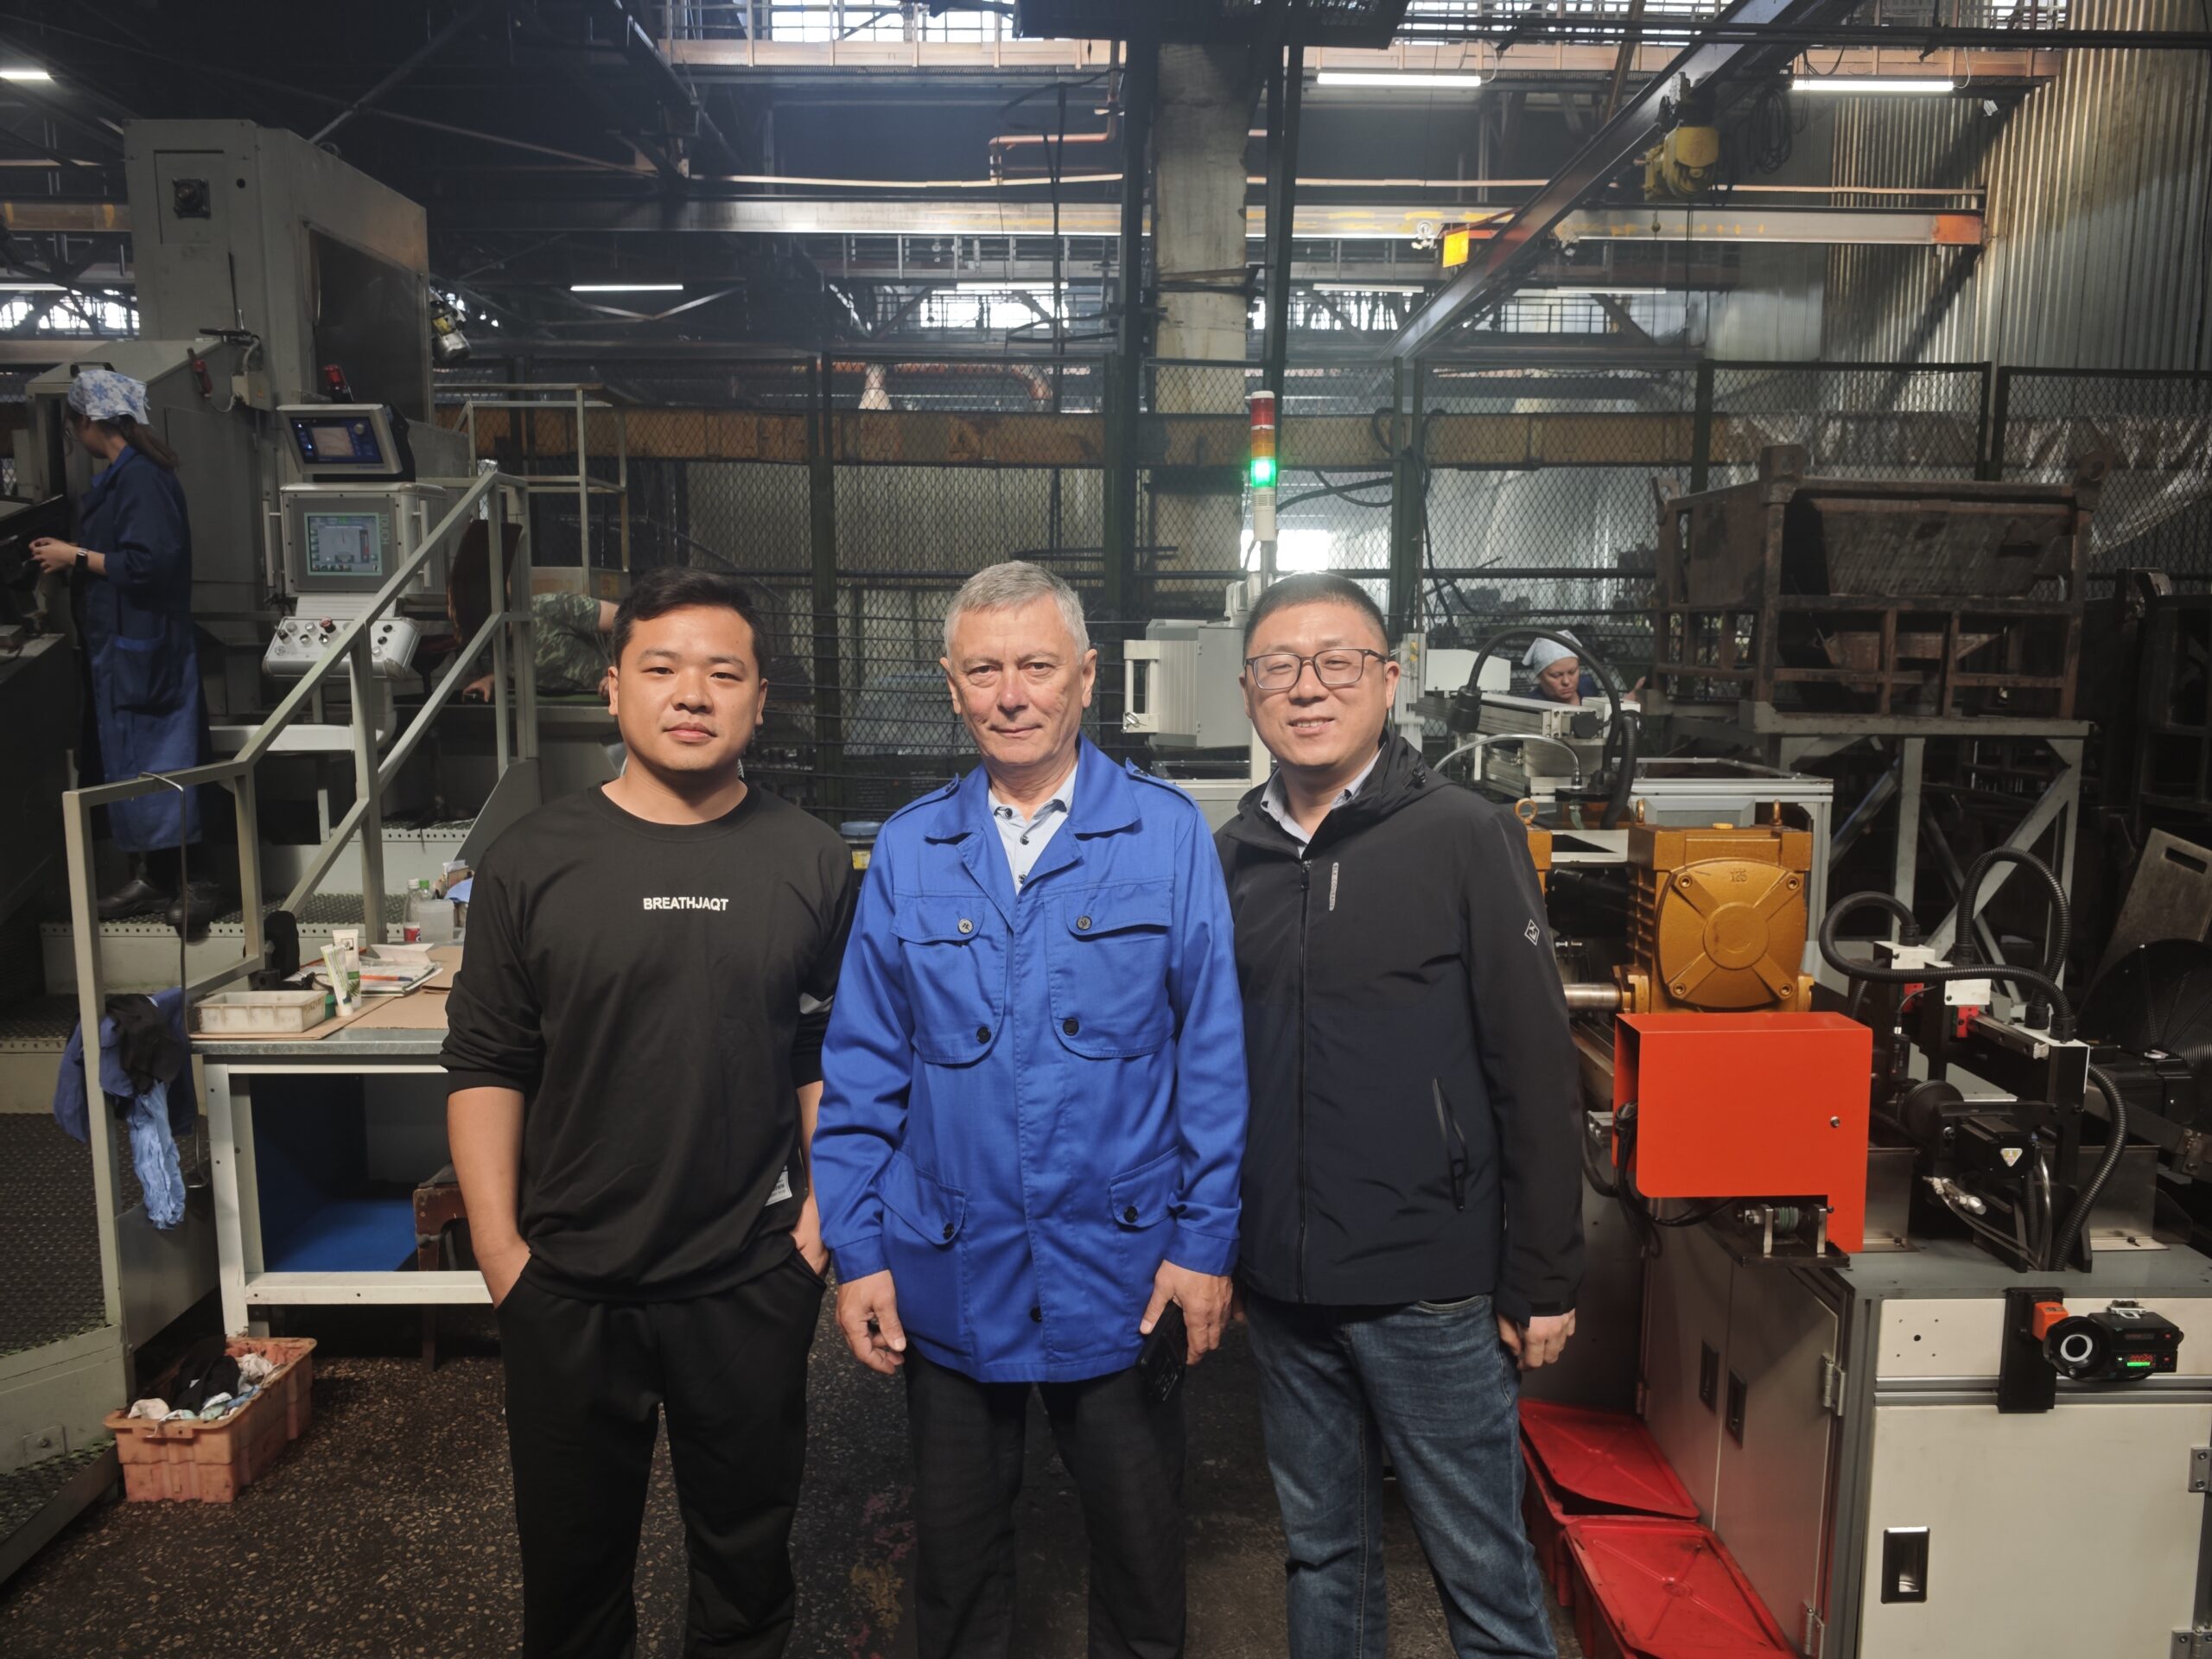
What a supplier needs before quoting is short and specific: the part drawing with its straightness callout and datum scheme, the material and heat-treatment state, the incoming bend distribution (a sample lot measured, not described), the acceptance rule in its released or loaded form, and the volumes that set the cycle-time target. From that basis the machine configuration — press tonnage class, feed and orientation, gauging, triedenie — follows rather than leads.
Customer Case: Short Bolt Straightening for a Russian Machinery Builder
Balzan, a Russian machinery manufacturing company producing a range of mechanical equipment and parts, needed to straighten large volumes of short bolts to protect assembly quality. After comparing equipment and inspecting installations, they selected our short bolt straightening machine, and the delivered line was configured around their part family, stav tepelného spracovania, and acceptance checks. Our engineers worked through their production process with them, designed and commissioned the equipment, and provided operator training and after-sales support. Pri následnom použití, the customer reported the machine running to expectation on precision, operability, and maintenance access — atribúty, ktoré táto stránka popisuje technickými výrazmi uvedenými vyššie. The case is our own project record, offered as context, not as a laboratory result.
Bežné režimy porúch a ich prevencia
Štyri vzory predstavujú väčšinu problémov s kvalitou na vyrovnávacích linkách s krátkymi skrutkami, and each has a defined prevention.
- Unsorted incoming lots. Worst-case parts consume multiple correction attempts while the line tunes itself chasing their scatter. Prevencia: a defined incoming check, parts grouped by bend severity before feed.
- Invisible press-tooling wear. A worn or chipped die face starts marking threads long before it stops correcting. Prevencia: tooling identity, wear criteria in the setup record, requalification after every change.
- Undefined acceptance state. Parts measured in the fixture pass; parts measured free at the customer fail, because nobody wrote down which state governs. Prevencia: state the released-state rule on the drawing and in the control plan.
- Retry habits. An operator re-running a part until the gauge passes erodes both the part's fatigue margin and the line's data. Witels Albert's glossary is the technical reason: the Bauschinger effect's magnitude depends on "the number of load cycles" — every extra press is a new load history. Prevencia: correction-attempt limits exist as policy, not preference.
FAQ
Can a long-bolt straightening machine also process short bolts?
Only within a validated overlap, and rarely well. The two families reward different machine investments — scanning and mapped correction for long parts, presné lokalizované lisovanie a rýchle meranie pre krátke. Uveďte režim, v ktorom vaše časti žijú, and let the sample test confirm the machine's fit for that regime.
V akom stave by mali byť skrutky pred vyrovnaním?
Čistý, identifikované podľa šarže a stavu tepelného spracovania, a zoskupené podľa závažnosti ohybu tam, kde to objemy dovoľujú. Korekčný recept sa správa odlišne v závislosti od podmienok materiálu, a linka napájaná zmiešanými dávkami míňa svoju maržu na kompenzáciu rozptylu, ktorý mohla zachytiť prijímajúca kontrola.
Ako sú vlákna chránené počas automatickej korekcie?
Prostredníctvom dizajnu kontaktnej zóny: lisovací a podporný kontakt na hladkej stopke, nástroje zodpovedajúce sekcii, zaoblené hrany všade, kde sa povrch môže dotknúť, a podávacie cesty, ktoré zabraňujú vzájomnému brúseniu dielov. The proof is the inspection agreed before the trial — thread gauges and flank condition reviewed alongside the geometry result.
Kde sa nachádza táto stránka
Krátke skrutky nie sú malé dlhé skrutky: ich tuhosť, cycle economics, and machine architecture reward a dedicated configuration, ako je uvedené vyššie. Táto stránka dopĺňa trojdielnu sekvenciu — krátke skrutky tu, a automatické puzdro na vyrovnávanie skrutiek pre prípad všeobecnej automatizácie, a automatické vyrovnávanie dlhých skrutiek pre rodinu strojov s dlhými skrutkami.
Hodnotenie vyrovnávania krátkych skrutiek pre výrobnú linku? Start with our vyrovnávanie lisom vs vyrovnávanie valcom comparison and the straightening sample test acceptance sprievodca — potom contact our team to discuss your part family and acceptance checks before you request a quote.
References
- Pure-Bend and Over-Bend Straightening Theory for In-Plane Curved Beams with Symmetrical Section and Straightening Mechanism Analysis — Wang, MDPI Metals 12(8):1362, 2022; over-bend straightening theory, three-point multi-step mechanism, springback-based stroke, 1.5‰ straightness result on tubes.
- Novel Straightening-Machine Design with Integrated Force Measurement for Straightening of High-Strength Flat Wire — Bathelt et al., MDPI Sensors 23(22):9091, 2023; manual adjustment burden, integrated force measurement enabling feedback control.
- 8 Reasons Steel Parts Can Warp in Heat Treat — PMPA (Precision Machined Products Association); quench-distortion causes and the 0.125% dimensional-change rule of thumb for medium carbon alloy steels.
- ISO 4759-1:2000 Tolerances for fasteners — Part 1: Bolts, skrutky, studs and nuts — Product grades A, B and C — ISO 4759-1; tolerance selection for metric fasteners by product grade, shank straightness tolerance formulas, gauge examples in Annex C.
- Straightness Gage and Gaging for Bolts and Screws, B18.2.9-2010 (R2021) — ASME; gage and gaging procedure for checking bolt or screw straightness at maximum material condition (MMC).
- Bauschingerov efekt — Wire Straightening Glossary — Witels Albert; definition of the Bauschinger effect and the factors governing its magnitude, including load cycles.
- Zákaznícka stránka stroja na vyrovnávanie dlhých skrutiek — YouTube; customer-site video of the long-bolt straightening machine family, linked in the comparison section above.