Tartalomjegyzék
- Ami valójában hajlítja a csavarokat
- Short Bolt Straightening vs Long-Bolt Machines
- How to Make Good Bolt With Straightener Equipment: A korrekciós hurok
- What a Bolt Straightening Machine Must Do for Short Parts
- The Short-Bolt Straightening Solution in Practice
- Gyakori meghibásodási módok és megelőzésük
- GYIK
- Ahol ez az oldal található
- References
Ami valójában hajlítja a csavarokat
Short bolts leave heat treatment bent more often than anyone likes, and the fix is not a hammer and a bench block. How to make good bolt with straightener equipment — dedicated press-straightening machinery — is a discipline of measured bends, controlled strokes, and verified acceptance. It also differs from long-bolt work in ways that matter to anyone specifying a machine, because a part with almost no span between its head and its thread punishes the wrong equipment choice.
A csavar torzítása többnyire hőkezelési történet, kezelési epilógussal. A kioltás egyenetlenül hűti le az alkatrészt, feszültségekbe zárja, és a rész meghajol, amikor ezek a stresszek ellazulnak. The Precision Machined Products Association (PMPA) separates the two distortion modes plainly: dimensional change from phase transformation is expected and small, while warpage "is usually a result of process and design issues." Their heat-treat guidance lists eight recurring causes of warp on quench and temper — from rapid heating and non-uniform cooling to water contamination in the quench oil, large changes of mass and section, and asymmetric features — and explains the mechanism: "Non-uniform cooling allows unbalanced stresses to develop during the quench, as does non-uniform agitation of quench medium."
For sizing expectations, PMPA offers a working rule of thumb for medium carbon alloy steels: "a change in linear dimensions of about 0.125% maximum" from heat treatment and quench. That is the scale of the distortion budget before warpage even enters the picture. Thread rolling and machining add their own residual-stress history on top, which is why finished fasteners arrive at the straightening station with bends that no amount of careful handling will prevent.
Short bolts then add a twist of their own. Egy rövid csavar merevebb, mint egy azonos átmérőjű hosszú, so it bends less from a given stress — but everything around it is tighter. The thread must gauge, the assembly must seat, and there is little room even for modest bows. The underlying mechanics of how prior deformation changes a part's response to correction — reverse loading and the Bauschinger hatás — matter here as much as anywhere in straightening work.
Key takeaways
- Bolt bend is mainly a quench-distortion problem: non-uniform cooling and agitation leave unbalanced stresses that relax into a bow.
- Heat-treat dimensional change alone runs up to about 0.125% of linear dimensions on medium carbon alloy steels, per PMPA's rule of thumb.
- Short bolts are stiff but unforgiving: tighter effective tolerances and almost no span for correction make machine choice decisive.
Short Bolt Straightening vs Long-Bolt Machines
Csábító elképzelni egyetlen univerzális csavarkiegyenesítőt, de a fizika széttolja a két családot. Egy hosszú, karcsú csavar úgy viselkedik, mint egy tengely: előnyös a teljes hosszában történő szkennelés, a hajlítási görbe feltérképezése, and correcting at the mapped peaks — the approach behind our automatizált csavarkiegyenesítő megoldás for the general automation case and the automatikus hosszú csavar kiegyenesítési folyamat. The research mechanics of that correction style are well established: Wang's over-bend straightening theory, published in the MDPI journal Metals be 2022, describes how "a zigzag straightening moment was applied in the three-point multi-step straightening process to approximate the smooth curve of theoretical moment" — in other words, long-part machines press at discrete mapped points, stepping along the length.
Watch the long-bolt machine family running at a customer site on YouTube: Hosszú csavar egyengető gép ügyféloldala — scan the length, térképezze fel a kanyart, press at the mapped peaks, újra mérni. A short bolt offers almost no usable span between its head and thread, so the correction window is narrow from the start. Positioning accuracy of the part, precision of the press stroke, and protection of the thread zones dominate the result, while the bend map itself is simpler. Ezért a rövidcsavaros gépek az előtolásra koncentrálnak, tájolás, precise localized correction, and fast gauging, míg a hosszú csavaros rendszerek a szkennelésbe és a többpontos stratégiába fektetnek be.
Buyers specifying equipment should name which regime their parts live in. A machine optimized for one will process the other disappointingly — and for shaft-family parts beyond bolts, the same reasoning shapes our shaft straightening solutions.
How to Make Good Bolt With Straightener Equipment: A korrekciós hurok
The process flow on any short-bolt line reads the same — terhelés, pozíció, kiegyenesedik, teszt, discharge — but the engineering lives inside each step. The loop below is how the sequence earns its result.
Positioning Sets the Accuracy Budget
A pozicionálás az, ahol a legtöbb pontosság dől el. A bolt seated a fraction of a millimeter off its intended rotation axis reads as bent and gets corrected for a setup error, tehát dátum jellemzők, seating cleanliness, and repeat-clamping behavior are the accuracy foundation of the whole line. Before a single press stroke, the fixture must present the same part, on the same datum, the same way, every cycle.
The Straightening Press Stroke
A kiegyenesedés a legrövidebb lépés és a legkevésbé megbocsátó. The stroke is small, the response depends on the material's state, and the target follows from measured curvature: Wang's 2022 analysis builds the stroke on "the springback theory of small curvature plane bending," with the over-bend moment computed section by section. In the same paper's tube-straightening experiments, "the straightness of the straightened workpiece could be controlled within 1.5‰, which meets the standard requirements" — a research result on tubes, not a universal machine spec, but a measured anchor for what curvature-based stroke control achieves.
Over-correction on a short part is expensive because there is little span left for a counter-move. Each reverse press works the material again, and the accumulated load history changes how the next stroke behaves.
The Bauschinger Effect and the Cost of Over-Correction
Why does a part respond differently to its second press than its first? A Bauschinger-effektus. Witels Albert, a straightening-roll specialist, defines it in their Wire Straightening Glossary as "a change of material parameters due to a reversal of loading direction between two consecutive loads (például. tension/compression)." Straightening is exactly such a reversal, which is why correction recipes cannot treat the second press like the first. The same glossary notes the magnitude depends on the material, its alloying elements (particularly carbon), "the number of load cycles, and the dimensions of external deformation (actual strains)" — two of the four factors sit under the process engineer's control, which is the entire argument for correction-attempt limits as policy. Our companion article on a Bauschinger-effektus az egyenesítésben develops the mechanics.
Thread Protection During Automated Correction
Threads are the finished surface that pays for everyone else's mistakes. Protection is a contact-zone design problem: press and support contact belongs on the plain shank, tooling conforms to the section, edges are radiused everywhere a surface could touch, and feed routes keep bulk-fed parts from grinding each other. The proof is the inspection agreed before any trial — thread gauges and flank condition reviewed alongside the geometry result. The same discipline drives our felületvédő szerszámok egyengetéshez practice.
Measuring and Accepting the Result
Straightness of finished bolts is not a matter of taste; it is standardized. ISO 4759-1 "specifies a selection of tolerances for bolts, csavarok, studs and nuts with ISO metric threads and with product grades A, B and C," and its product grades are ordered: "grade A is the most precise and grade C is the least precise." For shank straightness the standard gives tolerance formulas that scale with length — for shanks up to 8 mm átmérőjű, t = 0.002 l + 0.05 mm; above 8 mm, t = 0.0025 l + 0.05 mm — so a 60 mm long M8 shank carries a straightness tolerance of about 0.17 mm by direct arithmetic. On the gaging side, ASME B18.2.9 "describes a gage and gaging procedure for checking bolt or screw straightness at maximum material condition (MMC)."
Two measurement disciplines protect the acceptance decision itself: minden alkatrész mérése javítás után, a megfelelő és nem megfelelő részekkel fizikailag elválasztva, szerint NOK rendezés és átdolgozás-limit keretrendszer — and defining the acceptance measure before gauging, because straightness, runout and TIR are not interchangeable terms; a miénk tengely egyenesség vs kifutás vs TIR primer separates them. Parts measured in the fixture that fail free at the customer are an acceptance-rule failure, not a machine failure.
What a Bolt Straightening Machine Must Do for Short Parts
Machine capability for this part family is concrete, not adjectival. On our UBJ-80 bolt straightening machine — a go-through straightener built for heat-treated finished parts including screws and fasteners — "the range of bar lengths is from 60 600 mm-ig, és az átmérők tartománya φ3~φ25mm," with a machining speed of "3~5 sec/piece." Those are this machine family's published figures, verified per lot against the drawing's straightness definition, not free-floating promises.
Two further capabilities separate a short-part line from a long-part one. Első, setup and adjustment burden: research on straightening-machine design (Bathelt et al., MDPI Sensors, 2023 — a flat-wire study) records that historically "the adjustment of a straightening machine has been performed manually, which is a lengthy and complex task even for an experienced worker," which is exactly the burden recipe management exists to remove on a high-mix short-part line. Második, sensor information: the same paper's contribution — an integrated, precise straightening force measurement that makes feedback control practical — is the direction short-bolt machine design follows, because a part pressed in seconds gives the process no time for manual re-tuning.
Incoming condition is the machine's silent partner. Lots identified by heat-treatment state and grouped by bend severity feed a stable correction recipe; a line fed mixed lots spends its margin compensating for scatter that receiving inspection could have caught.
The Short-Bolt Straightening Solution in Practice
What a supplier needs before quoting is short and specific: the part drawing with its straightness callout and datum scheme, the material and heat-treatment state, the incoming bend distribution (a sample lot measured, not described), the acceptance rule in its released or loaded form, and the volumes that set the cycle-time target. From that basis the machine configuration — press tonnage class, feed and orientation, gauging, osztályozás — follows rather than leads.
Customer Case: Short Bolt Straightening for a Russian Machinery Builder
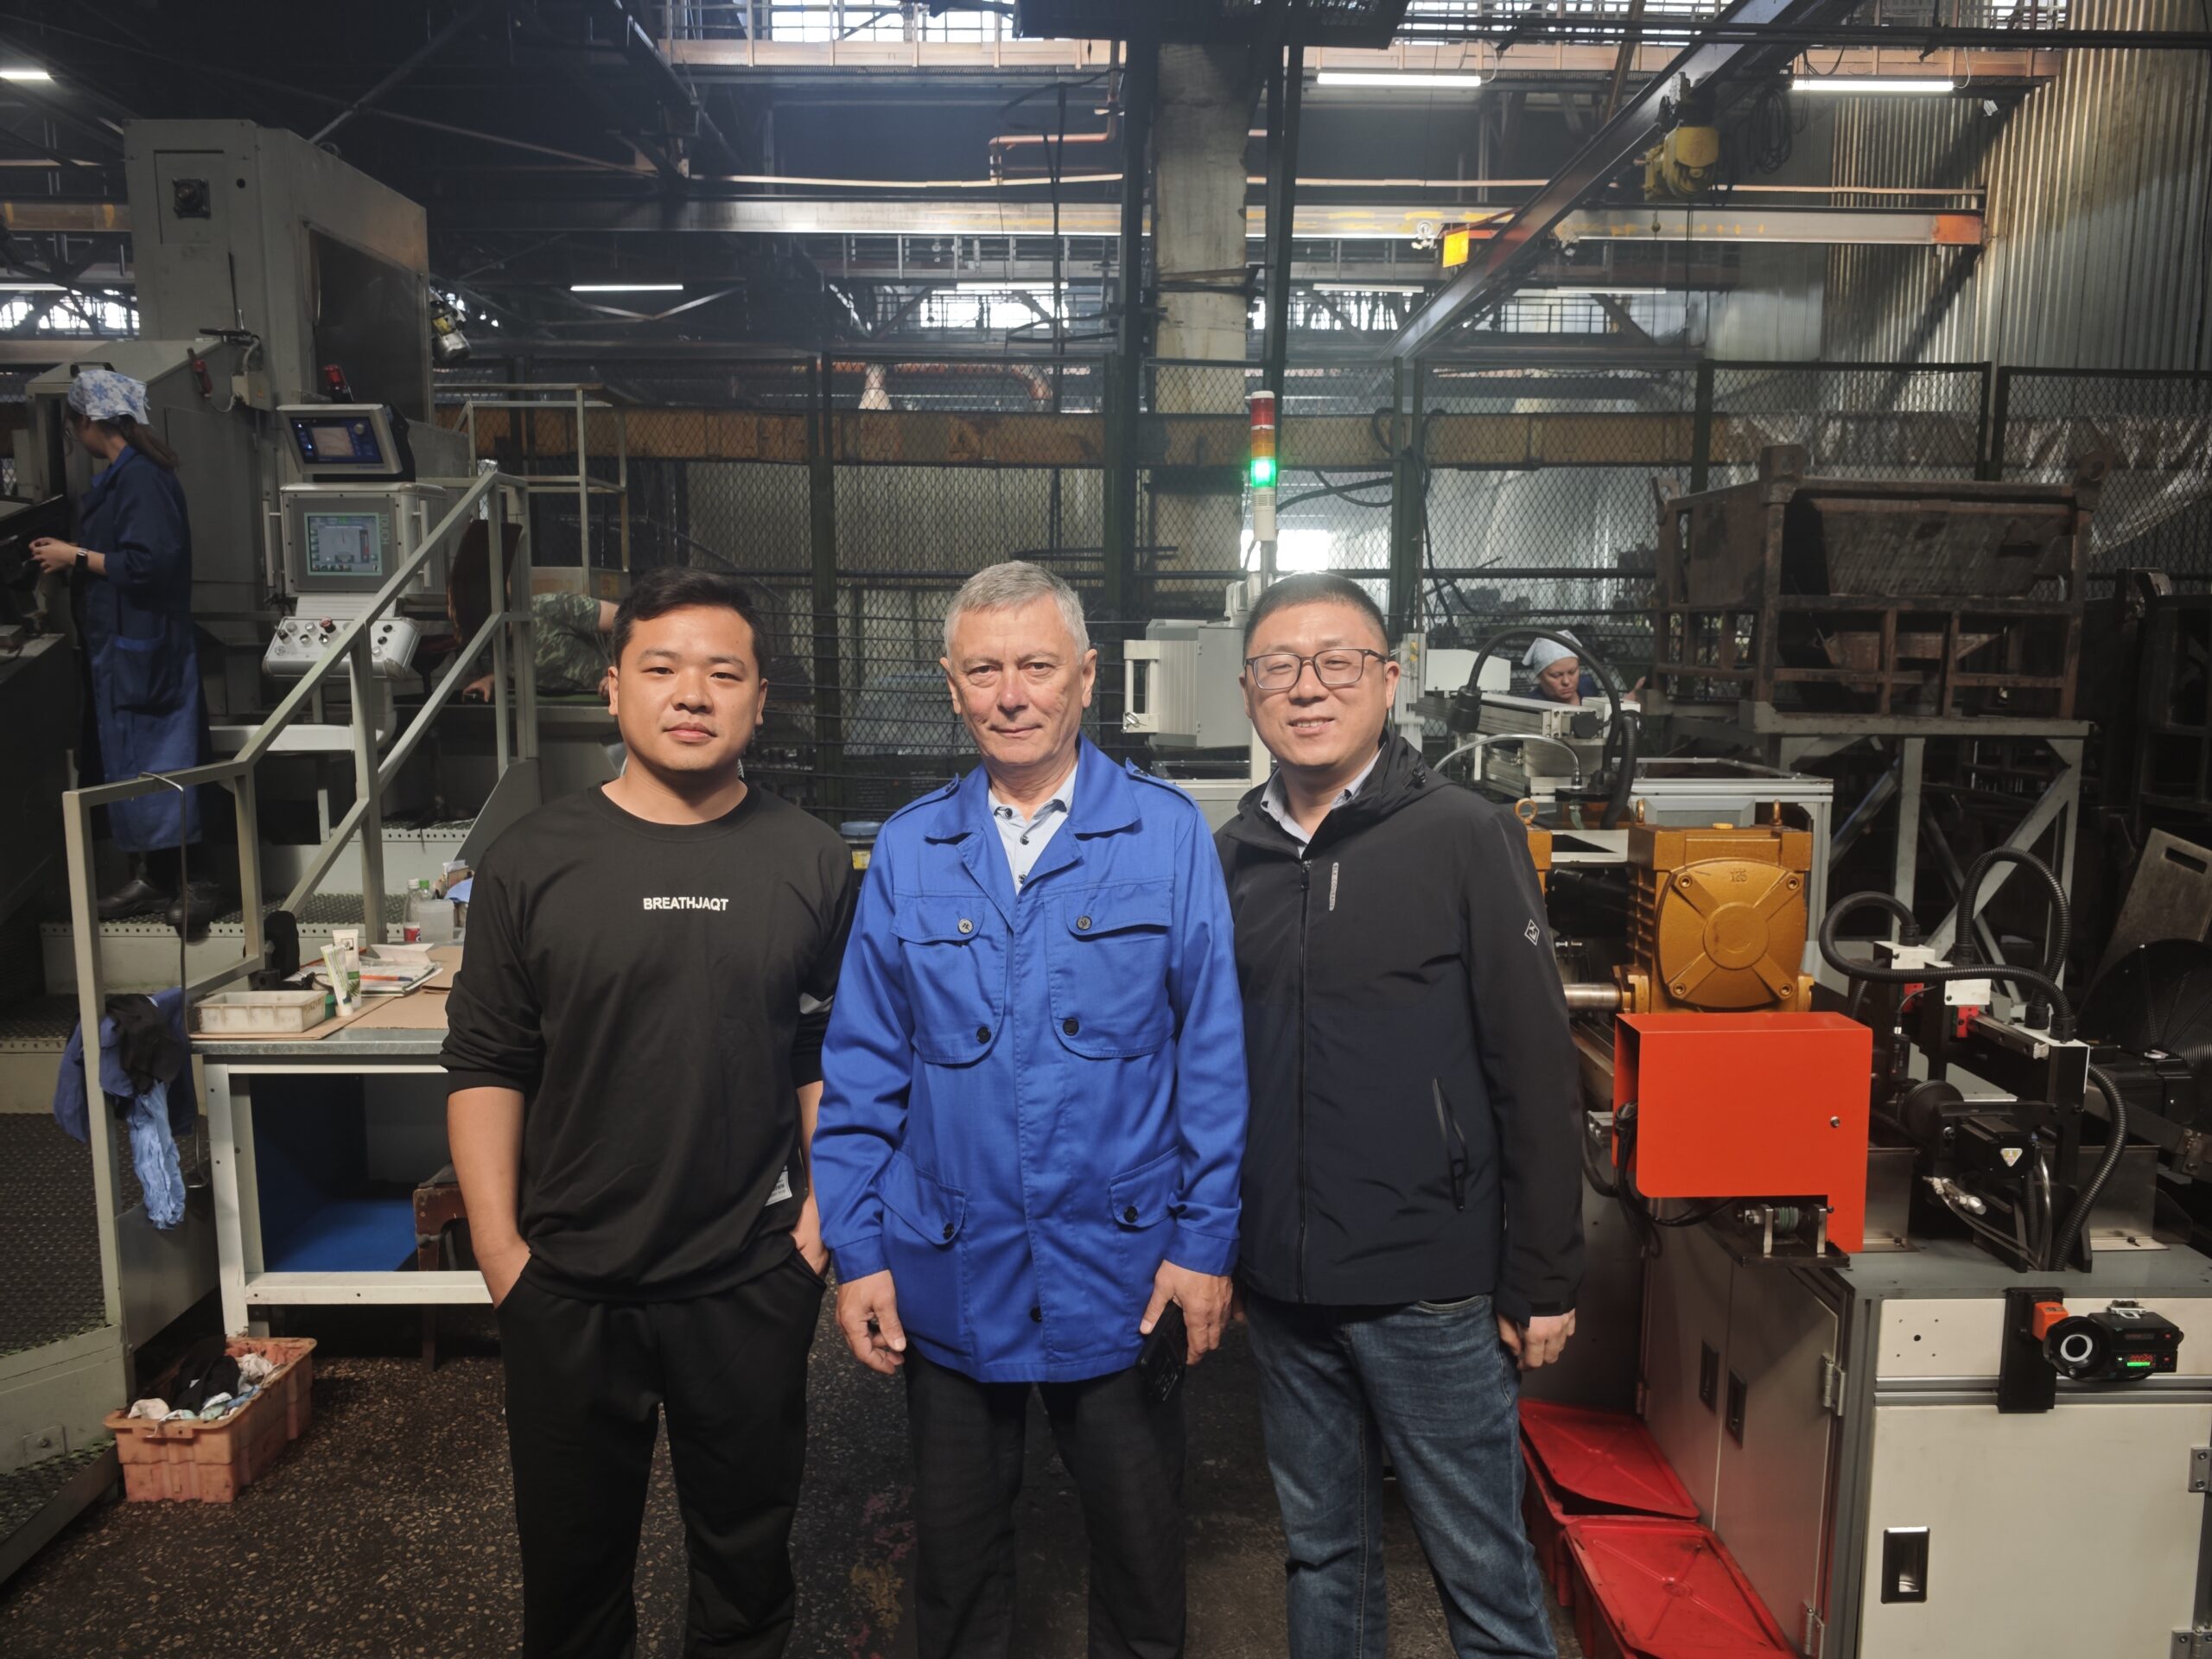
Balzan, a Russian machinery manufacturing company producing a range of mechanical equipment and parts, needed to straighten large volumes of short bolts to protect assembly quality. After comparing equipment and inspecting installations, they selected our short bolt straightening machine, and the delivered line was configured around their part family, hőkezelési állapot, and acceptance checks. Our engineers worked through their production process with them, designed and commissioned the equipment, and provided operator training and after-sales support. Utólagos használatban, the customer reported the machine running to expectation on precision, operability, and maintenance access — az ezen az oldalon leírt attribútumok mérnöki szempontból fent. The case is our own project record, offered as context, not as a laboratory result.
Gyakori meghibásodási módok és megelőzésük
Négy minta okozza a legtöbb minőségi problémát a rövid csavaros egyengető vonalakon, and each has a defined prevention.
- Unsorted incoming lots. Worst-case parts consume multiple correction attempts while the line tunes itself chasing their scatter. Megelőzés: a defined incoming check, parts grouped by bend severity before feed.
- Invisible press-tooling wear. A worn or chipped die face starts marking threads long before it stops correcting. Megelőzés: tooling identity, wear criteria in the setup record, requalification after every change.
- Undefined acceptance state. Parts measured in the fixture pass; az ügyfélnél szabadon mért alkatrészek meghibásodnak, because nobody wrote down which state governs. Megelőzés: state the released-state rule on the drawing and in the control plan.
- Retry habits. An operator re-running a part until the gauge passes erodes both the part's fatigue margin and the line's data. Witels Albert's glossary is the technical reason: the Bauschinger effect's magnitude depends on "the number of load cycles" — every extra press is a new load history. Megelőzés: correction-attempt limits exist as policy, not preference.
GYIK
Egy hosszú csavaros egyengetőgép képes-e rövid csavarokat is feldolgozni?
Csak érvényesített átfedésen belül, és ritkán jól. The two families reward different machine investments — scanning and mapped correction for long parts, precíz lokalizált préselés és gyors mérés a rövideknél. Adja meg azt a rezsimet, amelyben az alkatrészek élnek, and let the sample test confirm the machine's fit for that regime.
Milyen állapotban kell lenniük a csavaroknak egyengetés előtt?
Tiszta, tétel és hőkezelési állapot alapján azonosítják, és hajlítási súlyosság szerint csoportosítva, ahol a térfogatok lehetővé teszik. A korrekciós recept anyagi körülmények között eltérően viselkedik, és a vegyes tételekkel táplált zsinór árrését arra költi, hogy kompenzálja a szóródást, amelyet az ellenőrzés elkaphatott volna.
Hogyan védik a szálakat az automatikus javítás során??
Érintkezési zóna kialakításon keresztül: nyomja meg és támassza meg az érintkezőt a sima száron, metszetnek megfelelő szerszámozás, sugárzott élek mindenhol, ahol egy felület megérinthet, és olyan adagolási útvonalak, amelyek megakadályozzák, hogy az alkatrészek csiszolják egymást. The proof is the inspection agreed before the trial — thread gauges and flank condition reviewed alongside the geometry result.
Ahol ez az oldal található
A rövid csavarok nem kis hosszú csavarok: merevségük, cycle economics, and machine architecture reward a dedicated configuration, ahogy a fenti szakaszok megállapították. Ez az oldal egy három részből álló sorozatot fejez be — rövid csavarok itt, a automata csavarkiegyenesítő tok az általános automatizálási esethez, és automatikus hosszú csavar kiegyenesítés a hosszú csavaros gépcsaládhoz.
Gyártósor rövid csavarkiegyenesítésének értékelése? Start with our préses egyengetés vs görgős egyengetés comparison and the straightening sample test acceptance útmutató — majd contact our team to discuss your part family and acceptance checks before you request a quote.
References
- Pure-Bend and Over-Bend Straightening Theory for In-Plane Curved Beams with Symmetrical Section and Straightening Mechanism Analysis — Wang, MDPI Metals 12(8):1362, 2022; over-bend straightening theory, three-point multi-step mechanism, springback-based stroke, 1.5‰ straightness result on tubes.
- Novel Straightening-Machine Design with Integrated Force Measurement for Straightening of High-Strength Flat Wire — Bathelt et al., MDPI Sensors 23(22):9091, 2023; manual adjustment burden, integrated force measurement enabling feedback control.
- 8 Reasons Steel Parts Can Warp in Heat Treat — PMPA (Precision Machined Products Association); quench-distortion causes and the 0.125% dimensional-change rule of thumb for medium carbon alloy steels.
- ISO 4759-1:2000 Tolerances for fasteners — Rész 1: Bolts, csavarok, studs and nuts — Product grades A, B and C — ISO 4759-1; tolerance selection for metric fasteners by product grade, shank straightness tolerance formulas, gauge examples in Annex C.
- Straightness Gage and Gaging for Bolts and Screws, B18.2.9-2010 (R2021) — ASME; gage and gaging procedure for checking bolt or screw straightness at maximum material condition (MMC).
- Bauschinger hatás — Wire Straightening Glossary — Witels Albert; definition of the Bauschinger effect and the factors governing its magnitude, including load cycles.
- Hosszú csavar egyengető gép ügyféloldala — YouTube; customer-site video of the long-bolt straightening machine family, linked in the comparison section above.