Inhaltsverzeichnis
- Was Schrauben tatsächlich verbiegt
- Short Bolt Straightening vs Long-Bolt Machines
- How to Make Good Bolt With Straightener Equipment: Die Korrekturschleife
- What a Bolt Straightening Machine Must Do for Short Parts
- The Short-Bolt Straightening Solution in Practice
- Häufige Fehlerarten und ihre Vermeidung
- FAQ
- Wo sich diese Seite befindet
- References
Was Schrauben tatsächlich verbiegt
Short bolts leave heat treatment bent more often than anyone likes, and the fix is not a hammer and a bench block. How to make good bolt with straightener equipment — dedicated press-straightening machinery — is a discipline of measured bends, controlled strokes, and verified acceptance. It also differs from long-bolt work in ways that matter to anyone specifying a machine, because a part with almost no span between its head and its thread punishes the wrong equipment choice.
Die Bolzenverformung ist größtenteils eine Wärmebehandlungsgeschichte mit einem Nachwort zur Handhabung. Durch das Abschrecken wird das Teil ungleichmäßig abgekühlt, sperrt Spannungen ein, und das Teil verbiegt sich, wenn diese Spannungen nachlassen. The Precision Machined Products Association (PMPA) separates the two distortion modes plainly: dimensional change from phase transformation is expected and small, while warpage "is usually a result of process and design issues." Their heat-treat guidance lists eight recurring causes of warp on quench and temper — from rapid heating and non-uniform cooling to water contamination in the quench oil, large changes of mass and section, and asymmetric features — and explains the mechanism: "Non-uniform cooling allows unbalanced stresses to develop during the quench, as does non-uniform agitation of quench medium."
For sizing expectations, PMPA offers a working rule of thumb for medium carbon alloy steels: "a change in linear dimensions of about 0.125% maximum" from heat treatment and quench. That is the scale of the distortion budget before warpage even enters the picture. Thread rolling and machining add their own residual-stress history on top, which is why finished fasteners arrive at the straightening station with bends that no amount of careful handling will prevent.
Short bolts then add a twist of their own. Eine kurze Schraube ist steifer als eine lange mit demselben Durchmesser, so it bends less from a given stress — but everything around it is tighter. The thread must gauge, the assembly must seat, and there is little room even for modest bows. The underlying mechanics of how prior deformation changes a part's response to correction — reverse loading and the Bauschinger-Effekt — matter here as much as anywhere in straightening work.
Key takeaways
- Bolt bend is mainly a quench-distortion problem: non-uniform cooling and agitation leave unbalanced stresses that relax into a bow.
- Heat-treat dimensional change alone runs up to about 0.125% of linear dimensions on medium carbon alloy steels, per PMPA's rule of thumb.
- Short bolts are stiff but unforgiving: tighter effective tolerances and almost no span for correction make machine choice decisive.
Short Bolt Straightening vs Long-Bolt Machines
Es ist verlockend, sich einen universellen Bolzenrichtapparat vorzustellen, Doch die Physik treibt die beiden Familien auseinander. Entlang, Der schlanke Bolzen verhält sich wie eine Welle: Es profitiert vom Scannen in voller Länge, Abbildung der Biegekurve, and correcting at the mapped peaks — the approach behind our automatisierte Lösung zum Richten von Schrauben for the general automation case and the Automatischer Langbolzenrichtprozess. The research mechanics of that correction style are well established: Wang's over-bend straightening theory, published in the MDPI journal Metals In 2022, describes how "a zigzag straightening moment was applied in the three-point multi-step straightening process to approximate the smooth curve of theoretical moment" — in other words, long-part machines press at discrete mapped points, stepping along the length.
Watch the long-bolt machine family running at a customer site on YouTube: Kundenstandort einer Richtmaschine für lange Bolzen — scan the length, Kartieren Sie die Kurve, press at the mapped peaks, neu messen. A short bolt offers almost no usable span between its head and thread, so the correction window is narrow from the start. Positioning accuracy of the part, precision of the press stroke, and protection of the thread zones dominate the result, while the bend map itself is simpler. Deshalb konzentrieren sich Kurzbolzenmaschinen auf das Futter, Orientierung, precise localized correction, and fast gauging, während Langbolzensysteme in Scanning und Mehrpunktstrategie investieren.
Buyers specifying equipment should name which regime their parts live in. A machine optimized for one will process the other disappointingly — and for shaft-family parts beyond bolts, the same reasoning shapes our shaft straightening solutions.
How to Make Good Bolt With Straightener Equipment: Die Korrekturschleife
The process flow on any short-bolt line reads the same — laden, Position, begradigen, prüfen, discharge — but the engineering lives inside each step. The loop below is how the sequence earns its result.
Positioning Sets the Accuracy Budget
Der größte Teil der Genauigkeit wird über die Positionierung bestimmt. A bolt seated a fraction of a millimeter off its intended rotation axis reads as bent and gets corrected for a setup error, also Bezugsmerkmale, seating cleanliness, and repeat-clamping behavior are the accuracy foundation of the whole line. Before a single press stroke, the fixture must present the same part, on the same datum, the same way, every cycle.
The Straightening Press Stroke
Das Aufrichten ist der kürzeste und am wenigsten nachsichtige Schritt. The stroke is small, the response depends on the material's state, and the target follows from measured curvature: Wang's 2022 analysis builds the stroke on "the springback theory of small curvature plane bending," with the over-bend moment computed section by section. In the same paper's tube-straightening experiments, "the straightness of the straightened workpiece could be controlled within 1.5‰, which meets the standard requirements" — a research result on tubes, not a universal machine spec, but a measured anchor for what curvature-based stroke control achieves.
Over-correction on a short part is expensive because there is little span left for a counter-move. Each reverse press works the material again, and the accumulated load history changes how the next stroke behaves.
The Bauschinger Effect and the Cost of Over-Correction
Why does a part respond differently to its second press than its first? Der Bauschinger-Effekt. Witels Albert, a straightening-roll specialist, defines it in their Wire Straightening Glossary as "a change of material parameters due to a reversal of loading direction between two consecutive loads (z.B. tension/compression)." Straightening is exactly such a reversal, which is why correction recipes cannot treat the second press like the first. The same glossary notes the magnitude depends on the material, its alloying elements (particularly carbon), "the number of load cycles, and the dimensions of external deformation (actual strains)" — two of the four factors sit under the process engineer's control, which is the entire argument for correction-attempt limits as policy. Our companion article on Der Bauschinger-Effekt beim Richten develops the mechanics.
Thread Protection During Automated Correction
Threads are the finished surface that pays for everyone else's mistakes. Protection is a contact-zone design problem: press and support contact belongs on the plain shank, tooling conforms to the section, edges are radiused everywhere a surface could touch, and feed routes keep bulk-fed parts from grinding each other. The proof is the inspection agreed before any trial — thread gauges and flank condition reviewed alongside the geometry result. The same discipline drives our Oberflächenschutzwerkzeuge zum Richten practice.
Measuring and Accepting the Result
Straightness of finished bolts is not a matter of taste; it is standardized. ISO 4759-1 "specifies a selection of tolerances for bolts, Schrauben, studs and nuts with ISO metric threads and with product grades A, B and C," and its product grades are ordered: "grade A is the most precise and grade C is the least precise." For shank straightness the standard gives tolerance formulas that scale with length — for shanks up to 8 mm Durchmesser, t = 0.002 l + 0.05 mm; above 8 mm, t = 0.0025 l + 0.05 mm — so a 60 mm long M8 shank carries a straightness tolerance of about 0.17 mm by direct arithmetic. On the gaging side, ASME B18.2.9 "describes a gage and gaging procedure for checking bolt or screw straightness at maximum material condition (MMC)."
Two measurement disciplines protect the acceptance decision itself: Messung jedes Teils nach der Korrektur, wobei konforme und nicht konforme Teile physisch getrennt sind, pro NOK-Sortierung und Nacharbeitslimit-Framework — and defining the acceptance measure before gauging, because straightness, runout and TIR are not interchangeable terms; unser Wellengeradheit vs. Rundlauf vs. TIR primer separates them. Parts measured in the fixture that fail free at the customer are an acceptance-rule failure, not a machine failure.
What a Bolt Straightening Machine Must Do for Short Parts
Machine capability for this part family is concrete, not adjectival. On our UBJ-80 bolt straightening machine — a go-through straightener built for heat-treated finished parts including screws and fasteners — "the range of bar lengths is from 60 bis 600mm, und der Durchmesserbereich reicht von φ3 bis φ25 mm," with a machining speed of "3~5 sec/piece." Those are this machine family's published figures, verified per lot against the drawing's straightness definition, not free-floating promises.
Two further capabilities separate a short-part line from a long-part one. Erste, setup and adjustment burden: research on straightening-machine design (Bathelt et al., MDPI Sensors, 2023 — a flat-wire study) records that historically "the adjustment of a straightening machine has been performed manually, which is a lengthy and complex task even for an experienced worker," which is exactly the burden recipe management exists to remove on a high-mix short-part line. Zweite, sensor information: the same paper's contribution — an integrated, precise straightening force measurement that makes feedback control practical — is the direction short-bolt machine design follows, because a part pressed in seconds gives the process no time for manual re-tuning.
Incoming condition is the machine's silent partner. Lots identified by heat-treatment state and grouped by bend severity feed a stable correction recipe; a line fed mixed lots spends its margin compensating for scatter that receiving inspection could have caught.
The Short-Bolt Straightening Solution in Practice
What a supplier needs before quoting is short and specific: the part drawing with its straightness callout and datum scheme, the material and heat-treatment state, the incoming bend distribution (a sample lot measured, not described), the acceptance rule in its released or loaded form, and the volumes that set the cycle-time target. From that basis the machine configuration — press tonnage class, feed and orientation, gauging, Sortierung — follows rather than leads.
Customer Case: Short Bolt Straightening for a Russian Machinery Builder
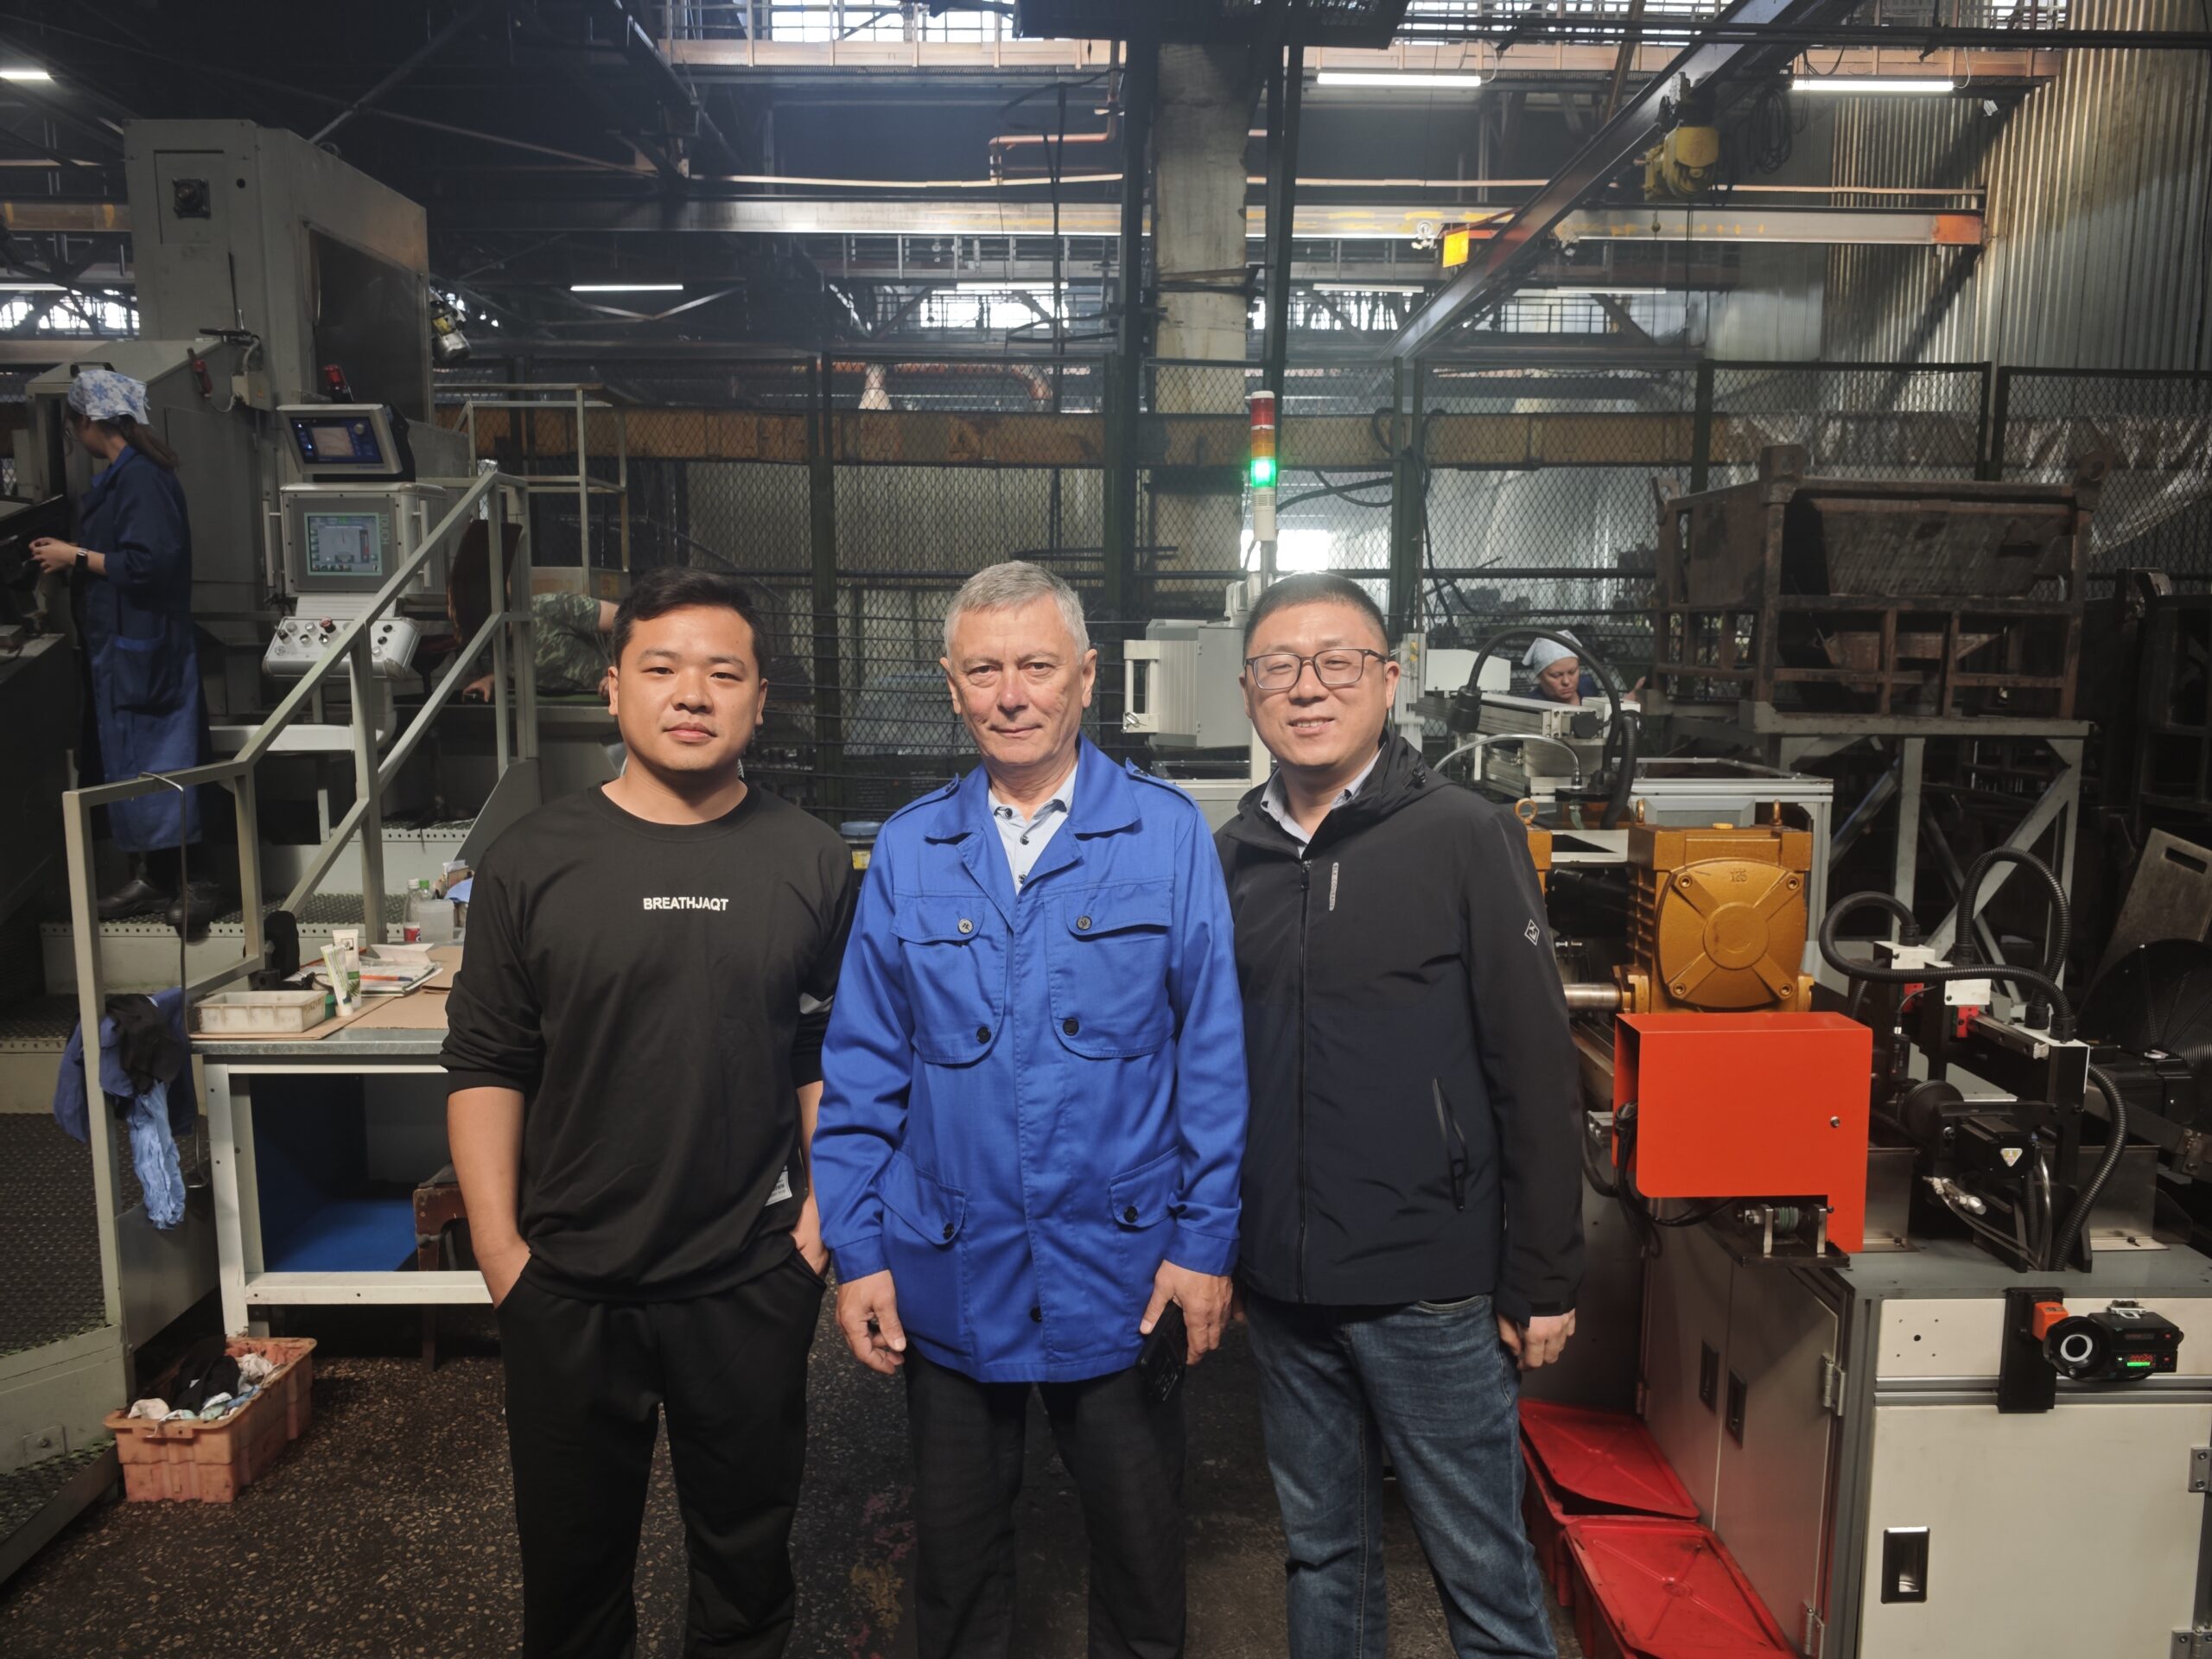
Balzan, a Russian machinery manufacturing company producing a range of mechanical equipment and parts, needed to straighten large volumes of short bolts to protect assembly quality. After comparing equipment and inspecting installations, they selected our short bolt straightening machine, and the delivered line was configured around their part family, Wärmebehandlungszustand, and acceptance checks. Our engineers worked through their production process with them, designed and commissioned the equipment, and provided operator training and after-sales support. Im Folgeeinsatz, the customer reported the machine running to expectation on precision, operability, and maintenance access — Die Attribute, die diese Seite oben in technischer Hinsicht beschreibt. The case is our own project record, offered as context, not as a laboratory result.
Häufige Fehlerarten und ihre Vermeidung
Vier Muster sind für die meisten Qualitätsprobleme bei Kurzbolzenrichtlinien verantwortlich, and each has a defined prevention.
- Unsorted incoming lots. Worst-case parts consume multiple correction attempts while the line tunes itself chasing their scatter. Verhütung: a defined incoming check, parts grouped by bend severity before feed.
- Invisible press-tooling wear. A worn or chipped die face starts marking threads long before it stops correcting. Verhütung: tooling identity, wear criteria in the setup record, requalification after every change.
- Undefined acceptance state. Parts measured in the fixture pass; Frei beim Kunden vermessene Teile fallen aus, because nobody wrote down which state governs. Verhütung: state the released-state rule on the drawing and in the control plan.
- Retry habits. An operator re-running a part until the gauge passes erodes both the part's fatigue margin and the line's data. Witels Albert's glossary is the technical reason: the Bauschinger effect's magnitude depends on "the number of load cycles" — every extra press is a new load history. Verhütung: correction-attempt limits exist as policy, not preference.
FAQ
Kann eine Langbolzen-Richtmaschine auch kurze Bolzen bearbeiten??
Nur innerhalb einer validierten Überlappung, und selten gut. The two families reward different machine investments — scanning and mapped correction for long parts, Präzises lokales Pressen und schnelles Messen für kurze Pressen. Geben Sie das Regime an, in dem Ihre Teile leben, and let the sample test confirm the machine's fit for that regime.
In welchem Eingangszustand sollten sich die Schrauben vor dem Richten befinden??
Sauber, identifiziert durch Charge und Wärmebehandlungszustand, und nach Biegegrad gruppiert, sofern das Volumen dies zulässt. Das Korrekturrezept verhält sich je nach Materialbedingungen unterschiedlich, und ein liniengespeistes gemischtes Los gibt seine Marge aus, um die Streuung auszugleichen, die bei der Eingangskontrolle hätte auftreten können.
Wie werden Threads während der automatischen Korrektur geschützt??
Durch Kontaktzonengestaltung: Press- und Stützkontakt auf dem Schaft, Werkzeug entsprechend dem Abschnitt, Abgerundete Kanten überall dort, wo eine Oberfläche berühren könnte, und Zuführwege, die verhindern, dass Teile aneinander reiben. The proof is the inspection agreed before the trial — thread gauges and flank condition reviewed alongside the geometry result.
Wo sich diese Seite befindet
Kurze Bolzen sind keine kleinen langen Bolzen: ihre Steifheit, cycle economics, and machine architecture reward a dedicated configuration, wie in den obigen Abschnitten dargelegt. Diese Seite vervollständigt eine dreiteilige Sequenz — kurze Schrauben hier, Die Automatischer Bolzenrichtkoffer für den allgemeinen Automatisierungsfall, Und Automatisches Richten langer Bolzen für die Langbolzenmaschinenfamilie.
Bewertung des Richtens kurzer Bolzen für eine Produktionslinie? Start with our Pressrichten vs. Rollenrichten comparison and the straightening sample test acceptance Führung — Dann contact our team to discuss your part family and acceptance checks before you request a quote.
References
- Pure-Bend and Over-Bend Straightening Theory for In-Plane Curved Beams with Symmetrical Section and Straightening Mechanism Analysis — Wang, MDPI Metals 12(8):1362, 2022; over-bend straightening theory, three-point multi-step mechanism, springback-based stroke, 1.5‰ straightness result on tubes.
- Novel Straightening-Machine Design with Integrated Force Measurement for Straightening of High-Strength Flat Wire — Bathelt et al., MDPI Sensors 23(22):9091, 2023; manual adjustment burden, integrated force measurement enabling feedback control.
- 8 Reasons Steel Parts Can Warp in Heat Treat — PMPA (Precision Machined Products Association); quench-distortion causes and the 0.125% dimensional-change rule of thumb for medium carbon alloy steels.
- ISO 4759-1:2000 Tolerances for fasteners — Teil 1: Bolts, Schrauben, studs and nuts — Product grades A, B and C — ISO 4759-1; tolerance selection for metric fasteners by product grade, shank straightness tolerance formulas, gauge examples in Annex C.
- Straightness Gage and Gaging for Bolts and Screws, B18.2.9-2010 (R2021) — ASME; gage and gaging procedure for checking bolt or screw straightness at maximum material condition (MMC).
- Bauschinger-Effekt — Wire Straightening Glossary — Witels Albert; definition of the Bauschinger effect and the factors governing its magnitude, including load cycles.
- Kundenstandort einer Richtmaschine für lange Bolzen — YouTube; customer-site video of the long-bolt straightening machine family, linked in the comparison section above.