
Shaft straightening is not one universal machine process. A plain bar, stepped motor shaft, flanged axle, geared transmission shaft and long hollow drive shaft can all appear “bent,” but they do not share the same functional datum, safe contact zones, measuring method or correction response.
StraighteningTech evaluates shaft-straightening projects from the workpiece drawing, ubah bentuk masuk, process stage and acceptance method. This hub compares established shaft-straightening architectures and routes an inquiry; it does not state that every listed workpiece family or machine architecture is within our current verified supply range. A project-specific capability, cycle time and equipment configuration may be specified only after drawing review, korelasi tolok, representative testing and released acceptance results.
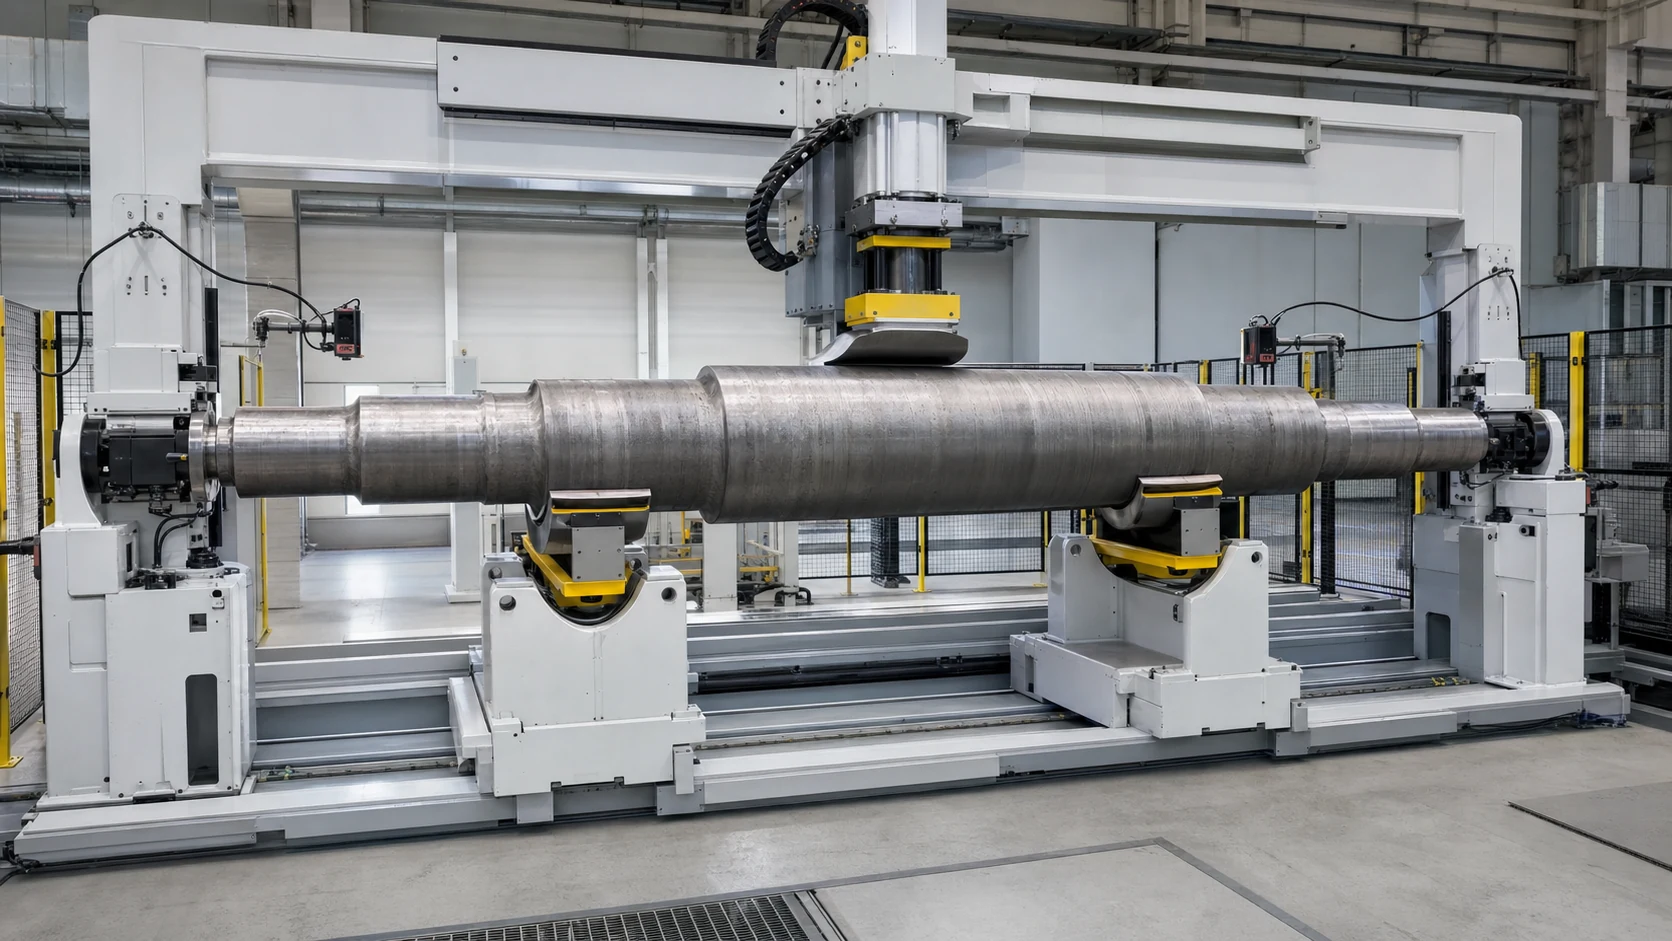
*Ilustrasi konsep kejuruteraan. It does not represent a delivered machine, customer project, verified sensor configuration, accuracy or cycle time.*
Find the Right Route for Your Shaft
Start with geometry and function. The useful question is not only “What is the shaft diameter?” but “Which features define the axis in the next machining or assembly operation?”
| Shaft Family | Typical Features | Primary Engineering Risk | Likely Starting Method |
|---|---|---|---|
| Plain shaft or bar blank | Constant diameter, unfinished surface | Long-span support and multiple bends | Roller straightening or point press, depending on length and tolerance |
| Stepped motor or pump shaft | Membawa jurnal, rotor seat, bahu, alur kunci | False runout from the wrong datum; marks on finished journals | Pengukuran automatik dan pelurus tekan titik |
| Kotak gear atau aci splined | Jurnal, gear, splines, lubang jejari | Runout berfungsi, pengukuran gigi dan zon sensitif retak | Pengukuran berbilang titik dan pembetulan titik terkawal |
| Gandar atau aci bebibir | Badan panjang, bebibir, spline, benang | Putaran stabil, datum bebibir dan kekakuan tidak simetri | Sokongan berdedikasi, putaran dan pembetulan titik |
| cacing, plumbum atau skru bola | Bahagian berfungsi berulir, jurnal, rentang langsing | Gangguan siasatan, kerosakan benang dan springback | Realisasi datum yang ditakrifkan lukisan—seperti jurnal yang diluluskan, pusat atau tolok berfungsi—dengan zon pembetulan yang dilindungi |
| Camshaft atau aci sipi | Lobus, jurnal dan bahagian perubahan | Permukaan pengukur yang tidak teratur dan perubahan kekakuan setempat | Pengukuran sedar ciri dan pembetulan khusus model |
| Aci pemacu berongga atau tiub | Dinding nipis, kimpalan, kuk atau bebibir | Runtuh, kemek, hubungan fasa dan interaksi imbangan | Alat pelindung tiub; straightening and balancing treated separately |
| Steering rack or asymmetric shaft | Smooth journals plus toothed rack | Bahagian bukan bulat, gear function and restricted press zones | Profile-aware support, measurement and correction |
If the part combines several families, the most sensitive functional feature controls the solution. A hollow splined drive shaft, contohnya, cannot be treated as a simple round bar.
These routes are screening hypotheses, not universal assignments. Lukisan itu, peringkat proses, permitted contact zones and representative trials decide the final method.
Define the Correct Measurement Before Straightening
Kelurusan, pelarian bulat, total runout and shop-floor TIR are related but not interchangeable. The drawing must identify the governing ISO or ASME system and edition. Straightness is a form control and does not use an external datum reference. Circular and total runout are evaluated relative to a specified datum axis; the physical support and machine rotation axis must be shown to realize that datum.
| Drawing Requirement | What Must Be Agreed | Why It Matters to the Machine |
|---|---|---|
| Axis or surface straightness | Controlled line, tolerance zone and evaluation length | Defines measuring positions and correction objective |
| Larian pekeliling | Paksi tarikh, permukaan kuar, axial station and one full rotation | Controls the reading at the specified circular section |
| Jumlah habis | Paksi tarikh, controlled surface, probe path and rotation rule | Extends evaluation across the specified surface |
| Shop-floor TIR | Datum, station or path, rotation and max–min reading rule | TIR must not be assumed to mean GD&T total runout |
| Journal-to-datum-axis relationship | Exact drawing characteristic, datum features and controlled journals | Avoids using “coaxiality” as an undefined shop-floor substitute |
| Gear or spline function | Pitch-diameter or functional gauge method | Smooth journal measurement alone may miss a functional error |
| Final assembly behavior | galas, meterai, gandingan, rotor or gear interfaces | Prevents optimizing a convenient dimension that does not control the assembly |
Sebelum sebut harga, mark every support, measuring and pressing zone on the drawing. Also mark keyways, alur, benang, lubang minyak, cross holes, lobes, gigi, thin walls, kimpalan, coatings and final-ground surfaces that must not be contacted without approval.
For results near the tolerance boundary, the machine and customer methods should document the same measurand and measurement model, together with the applicable uncertainty and conformity decision rule.
Point Press or Roller Straightening?
The choice depends on geometry, process stage and acceptance method—not on a generic preference for one machine type.
| Faktor Keputusan | Automatic Point Press Straightening | Roller or Through-Feed Straightening |
|---|---|---|
| Best starting fit | Discrete stepped or feature-rich shafts | Constant-section bars, tubes and shaft blanks |
| Pengukuran | Rotation at defined journals with one or more probes | Offline or integrated straightness/runout measurement |
| Pembetulan | Local controlled over-bending at an approved axial and angular position | Repeated bending through arranged rolls |
| Feature protection | High flexibility for no-press and no-support zones | Limited when steps, gear, flanges or finished features enter the rolls |
| Perubahan model | resepi, support and tooling changes | Roll setting, guide and line setup changes |
| Typical advantage | Closed-loop correction linked to the measured bend | Continuous processing and efficient handling of uniform material |
| Main validation need | Springback model, contact marks and maximum correction limits | Roll geometry, surface protection and full-length result |
Some production routes use both methods at different stages. A constant-diameter blank may be roller-straightened before machining, while the finished stepped shaft receives datum-based point correction after heat treatment or grinding.
Closed-Loop Automatic Shaft Straightening Process
For a feature-rich shaft, the common engineering sequence is measure, mengira, correct and remeasure. The exact sensors, menyokong, press force and automation modules are selected for the real part family.
The video shows one automatic small-shaft material-flow and press-straightening concept. It demonstrates visible equipment structure and sequence only; its public metadata does not establish a motor-shaft identity, jenis sensor, memaksa, tolerance or cycle time.
1. Kenal pasti Bahagian dan Pilih Resipi yang Disahkan
Resipi yang dicadangkan mentakrifkan realisasi datum, jawatan sokongan, stesen pengukur, zon pembetulan yang dibenarkan, ciri sasaran dan had pembetulan maksimum. Kod bar, DMC atau pemilihan pesanan pengeluaran ialah seni bina pilihan yang mungkin mengurangkan ralat model campuran apabila disertakan dalam skop projek yang disahkan.
2. Muatkan, Sokong dan Putar Aci
Pemuatan manual, sebuah dulang, penghantar, robot atau gantri ialah seni bina pengendalian calon dan bukannya skop lalai. Bahan kerja mesti berputar secara stabil dalam susunan sokongan yang disahkan yang merealisasikan datum yang ditentukan. Pusat-pusat, V-sokongan, penggelek dan paksi putaran mesin tidak boleh ditukar ganti secara automatik.
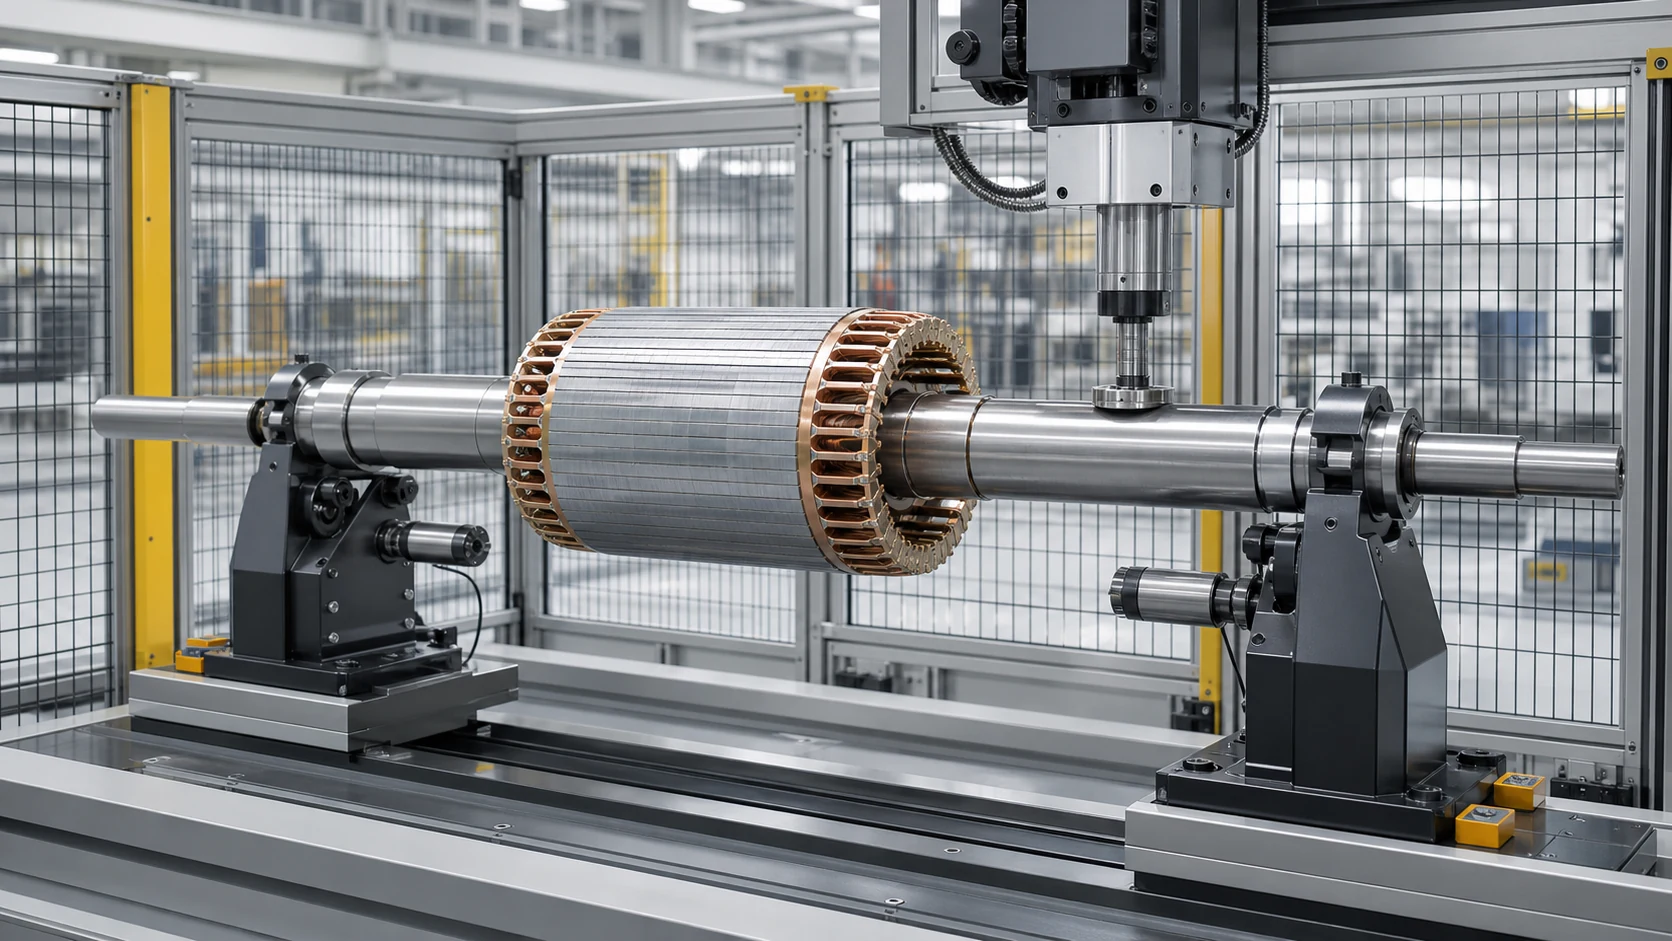
*Ilustrasi konsep kejuruteraan. Geometri adalah contoh saringan generik, tidak disahkan bahagian pelanggan StraighteningTech atau liputan mesin semasa.*
3. Ukur Sisihan Masuk
Kuar kenalan, penderia bukan kenalan atau tolok berfungsi merekodkan sisihan pada kedudukan yang diluluskan. Sistem harus membezakan selekoh sebenar daripada pencemaran, sebuah alur, peralihan diameter atau tempat duduk yang tidak stabil.
4. Kira Kedudukan dan Arah Pembetulan
Pengawal mengenal pasti kedudukan selekoh paksi dan sudut yang dominan. Untuk aci dengan beberapa selekoh, jujukan mesti mengelak daripada membetulkan satu lokasi sambil mencipta hasil yang tidak boleh diterima di lokasi lain.
5. Guna Lentur Terlalu Terkawal
Tekan hanya bergerak ke zon yang diluluskan dan membengkokkan aci melepasi kedudukan akhir yang diingini supaya springback elastik menjadikannya lebih dekat ke sasaran. Strok dan, di mana sesuai, had daya dibangunkan daripada tindak balas sampel.
6. Ukur Semula dan Putuskan
Datum dan stesen pengukur yang sama digunakan semula. If the result remains outside target but stays within validated correction limits, another controlled correction may be allowed. Parts that reach a cycle, strok, force or plausibility limit are sent to NOK or engineering review.
7. Rakam dan Punggah
If traceability is included in the confirmed control scope, a configured cell may store before/after values, resepi, correction count and OK/NOK result. The required data interface remains subject to project engineering and acceptance.
Protect Functional Features and Surfaces
A shaft can meet a runout value and still be unusable if the process marks a bearing journal, damages a thread, distorts a hollow wall or initiates a crack. Tooling and correction rules therefore need a feature-protection plan.
| Ciri | Typical Risk | Kawalan yang Diperlukan |
|---|---|---|
| Ground bearing or seal journal | Sokongan atau tanda tekan | Clean contoured contacts and approved contact pressure |
| Gear teeth or spline | Tooth damage or misleading probe signal | Functional measurement where required; no uncontrolled press contact |
| Alur kunci, alur atau lubang jejari | Stress concentration and crack initiation | Exclusion zone and conservative correction limits |
| Thread or worm section | Flank damage and unstable measurement | Measure on approved journals; protect threaded section |
| Bebibir | Unstable support or face distortion | Dedicated locating and support concept |
| Hollow or thin-wall section | Ovaliti, denting or collapse | Distributed support and tube-specific tooling |
| Peralihan yang mengeras | Brittle response or crack risk | Hardness/batch review, sample trials and stop limits |
| Coated or finished surface | Cosmetic or functional damage | Compatible contact materials and cleanliness control |
One Platform May Cover Multiple Shaft Models
A flexible cell may cover a shaft family when machine travel, force and sensor range overlap and change tooling can reproduce the correct datum. Model coverage must be proven across the complete envelope, not only on a nominal sample.
*Ilustrasi konsep kejuruteraan. It shows a possible released-state verification arrangement without claiming a datum, uncertainty, tolerance or accepted result.*
| Cell Module | Questions to Resolve |
|---|---|
| Base machine and press | Required travel, force/resolution window and correction access |
| Sokongan dan putaran | Datum, rentang, surface protection and model change method |
| Sistem pengukuran | Jenis sensor, number of stations, probe force and gauge correlation |
| Pengendalian | Manual, dulang, penghantar, gantri atau robot; orientation and buffer size |
| Kawalan | Recipe management, correction model, stop limits and abnormal-part logic |
| Quality data | Before/after values, kebolehkesanan, export and customer interface |
| Keselamatan | Menjaga, saling mengunci, overload protection and maintenance access |
Shaft Application Paths
This hub organizes shaft inquiries by workpiece because each family has different datum and feature-protection rules. Reviewed published examples currently include motor shafts, automotive axle shafts and small motor worm shafts. Other families—including textile shafts, lead or ball screws, aci pemacu, pemutar, roller shafts, crankshafts, camshafts and piston rods—remain evaluation routes whose project fit must be established from direct evidence and representative samples. Railway axles, machine-tool spindles and plasticizing screws are not represented here as current verified StraighteningTech capabilities. Solid shaft, hollow tube and long bar identities must be confirmed before assigning a cylindrical workpiece to a solution family.
For reviewed published examples, lihat Penyelesaian Meluruskan Aci Motor Automatik, Penyelesaian Meluruskan Aci Gandar Automotif dan Penyelesaian Meluruskan Aci Cacing Motor Kecil. Each new project still requires its own drawing and sample review.
Sample Validation Before a Final Proposal
Representative trials convert a machine concept into a defendable project specification. The sample set should include short/long, small/large diameter, normal/worst incoming bend, and relevant material or heat-treatment batches.
| Item Pengesahan | Bukti untuk Rekod |
|---|---|
| Measurement agreement | Datum, kedudukan kuar, gauge method and correlation result |
| Keadaan masuk | Pengagihan bengkok, surface state and abnormal samples |
| Respons pembetulan | Stroke/force response, springback and correction count |
| Final result | All required measuring stations, not only the worst initial point |
| Bahagian integriti | Tanda kenalan, retak, thread/tooth/flange condition and other risks |
| Production fit | Memuatkan, tukar ganti, cycle distribution, NOK handling and data needs |
| Sempadan penerimaan | Tested part family and conditions covered by the final quotation |
No universal accuracy or cycle-time claim applies to every shaft. A final guarantee should state the workpiece family, peringkat proses, julat masuk, datum, kaedah mengukur, sample evidence and acceptance conditions.
Information Needed for a Shaft Straightening Proposal
Sila berikan:
- 2D melukis dan, if available, 3model D;
- shaft material, kekerasan dan keadaan rawatan haba;
- minimum/maximum diameter, length and model matrix;
- pusat-pusat, membawa jurnal, tempat duduk rotor, gear, splines, bebibir, threads and other functional features;
- selekoh masuk atau agihan runout, termasuk kes terburuk;
- required characteristic, toleransi, datum and customer inspection method;
- sokongan yang dibenarkan, measuring and pressing zones;
- sensitive surfaces and prohibited contact areas;
- current process stage and next manufacturing or assembly step;
- jumlah pengeluaran, target takt jam, loading direction and changeover needs;
- representative samples covering the full family.
Soalan Lazim
Can one shaft straightening machine handle every shaft type?
Tidak. A platform can cover a validated family when its travel, memaksa, penderia, supports and tooling match the complete envelope. A geared, bebibir, hollow or highly slender shaft may need a different measuring or correction concept.
Is straightness the same as TIR?
Tidak. Straightness is a datum-independent form control. A TIR reading is a shop-floor max–min indication whose datum, probe station or path, rotation and reading rule must be documented; it is not automatically GD&T total runout. The drawing and customer gauge method must determine what the machine measures and accepts.
Should a stepped shaft use a roller straightener?
Roller straightening is a common starting candidate for constant-section material. After functional features are finished, a stepped shaft may instead require datum-based measurement, protected contact zones and local point correction; the drawing and sample trials decide the route.
Can hardened shafts be straightened without cracks?
It may be feasible, tetapi kekerasan, geometri, stress concentrations and incoming bend change the risk. Conservative correction limits, representative trials and crack or surface inspection requirements must be agreed.
Does shaft straightening replace balancing?
Tidak. Straightening controls geometry or runout; balancing controls mass distribution during rotation. A drive shaft or rotor may require both processes, with a defined sequence and separate acceptance criteria.
Apakah cara terpantas untuk menerima cadangan yang berguna?
Hantar lukisan itu, bahan/kekerasan, incoming and target measurements, datum, zon terlindung, production requirement and representative samples. This allows the engineering team to recommend a process and machine concept instead of guessing from diameter and length.
Build the Solution from the Workpiece
The reliable route is workpiece classification, measurement definition, pemilihan kaedah, protected-zone design and sample validation. This prevents a machine from being selected around an incomplete tolerance statement or a convenient but non-functional datum.
Hubungi StraighteningTech with your shaft drawing and sample information. Our solution team can prepare a proposed measuring, pembetulan, handling and validation concept for engineering review; final scope remains subject to drawing and sample validation.
Sempadan Rujukan Teknikal
This hub uses public technical material from ISO/ASME dimensional specification frameworks and established straightening-machine manufacturers to describe industry terminology, workpiece families and possible process architectures. Those sources do not prove StraighteningTech machine range, penderia, control algorithms, ketepatan, masa kitaran, traceability functions or delivery history. Project-specific claims require StraighteningTech drawings, configuration records, representative trials and released acceptance evidence.