
We have completed sample testing for a client from South Korea: stepped medical drill bits held to a 0.05 mm rakhetskrav. This article is the engineering record of that trial – what the workpiece demanded, which decisions carried the result, and how the number was verified.
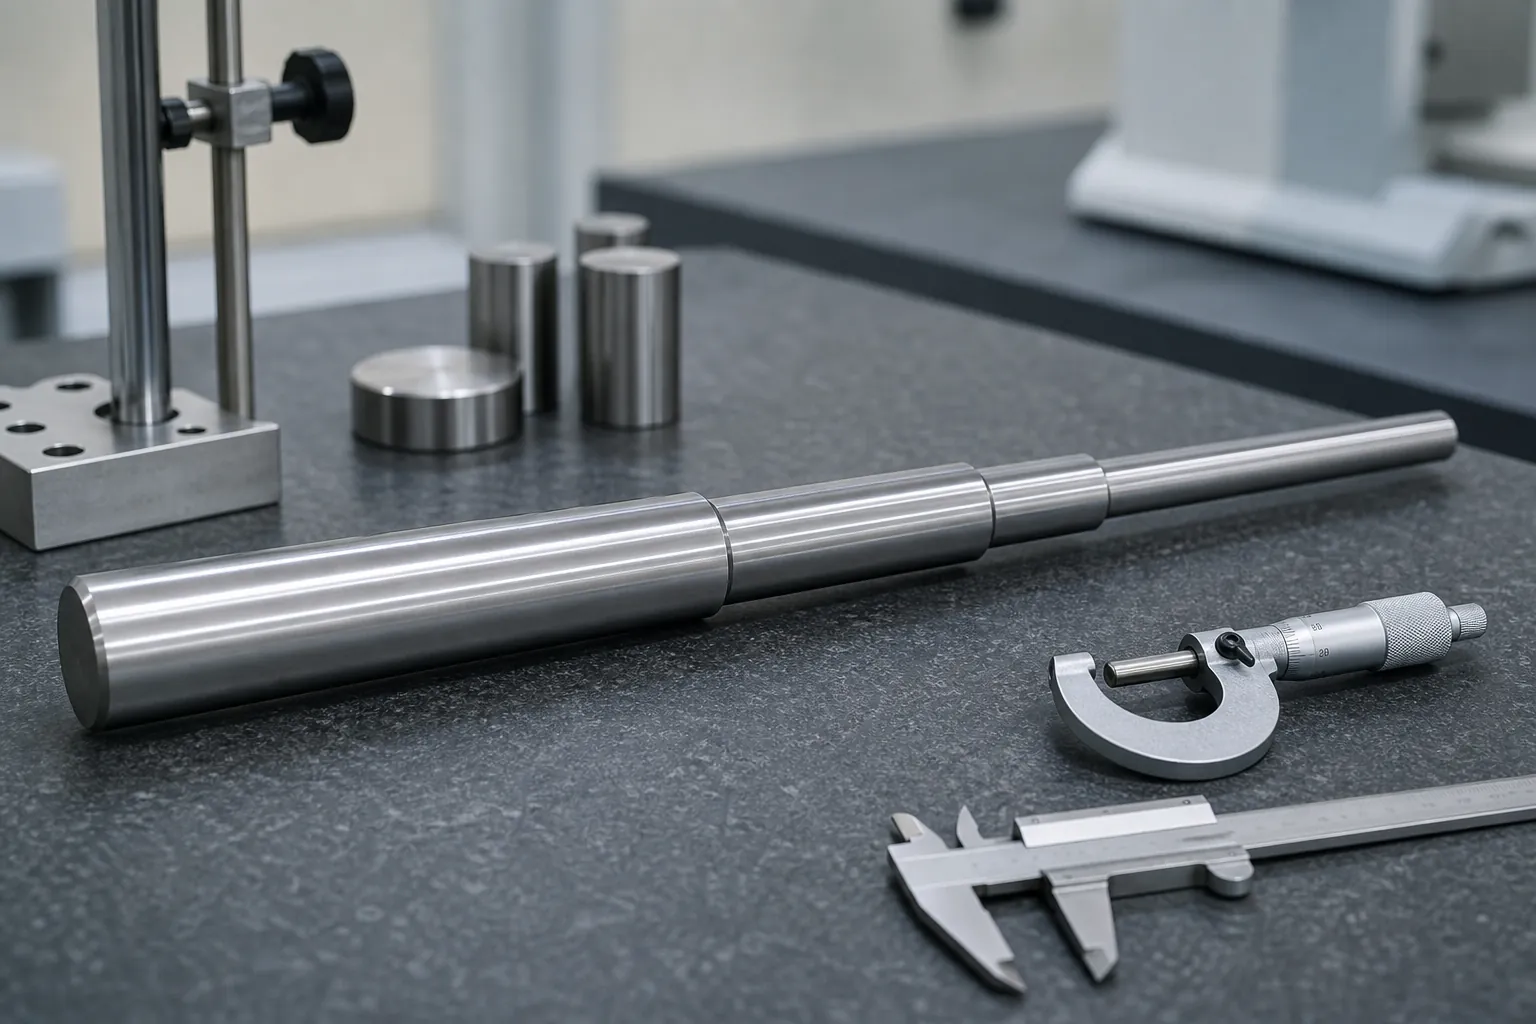
Utmaningen som de medicinska bitarna presenterar
Projektet involverade produktion av specialiserade medicinska bitar. Dessa komponenter hade en unik uppsättning specifikationer som utgör en betydande utmaning för våra maskiner och tekniska team. Arbetsstyckets dimensioner var just 7.9*230, och den innehöll en stavdiameter som avsmalnade från 7.9 – 6.9 – 5.9, med 3 distinkta steg längs dess längd. Sådana intrikata och exakta krav krävde den högsta nivån av noggrannhet och precision i våra tillverkningsprocesser.
Tillverkning av medicinska komponenter är ingen enkel prestation. Varje avvikelse från de nödvändiga specifikationerna kan potentiellt få allvarliga konsekvenser, särskilt inom det medicinska området där säkerhet och tillförlitlighet är av yttersta vikt. Vårt team var bra – medveten om tyngdkraften i uppgiften. Vi visste att vi var tvungna att dra ut alla stopp för att säkerställa att slutprodukten uppfyllde klientens strikta kvalitetsstandarder.
Engineering Review: Why a Stepped Medical Drill Is Hard to Straighten
Reading this project as engineers rather than storytellers, the workpiece specification explains the difficulty on its face. A 230 mm length stepping down through three diameters is not one slender rod but three slender rods joined in series, each with different stiffness. Correction force applied at one diameter produces different deflection per unit force at each step, the bend peak tends to sit near the stiffness transitions rather than at mid-length, and any measurement that treats the part as a uniform shaft misreads the geometry it is supposed to control. On top of the section problem, medical tooling acceptance is unforgiving: at a 0.05 mm rakhetskrav, the measurement method itself becomes a first-order participant, and the part’s function — a cutting instrument rotating predictably — leaves little room for the marks or residual distortion that a careless correction route would trade away for geometry.
Datum Selection Decides the Project Before the First Press
On a stepped shaft, which features define the measurement reference is not a detail — it is the project. Centering on the end center holes references the axis the part will rotate about in service; referencing the largest finished diameter makes the biggest section the anchor and reads the smaller steps against it; referencing a functional flank or flute zone answers what the tool actually needs straight, but demands feature-aware measurement. Each choice gives different numbers on the same part, so it must be agreed with the customer before trials, not discovered at acceptance. The framework for exactly this decision — including the reseating checks that prove the datum is being realized repeatably — is laid out for val av referenspunkt för stegvis axelmätning. For the sample test that then validates the correction route against that datum, the evidence rules in rätningsprov test och acceptans apply unchanged to medical tooling.
Step transitions deserve their own respect in the correction plan. The change of section concentrates stress at the shoulder, so correction strokes are planned to avoid loading a shoulder in bending where an alternative press location exists, and the flank surfaces of a cutting tool are treated as protected zones in the same discipline described for pistolborr och djuphålsborrriktning — the closest industrial cousin of this workpiece family.
How the Trial Was Executed
The trial work concentrated on two things: the correction plan for a 0.05 mm tolerance, and inspection between stages. Stödpositioner, press points and stroke settings were fixed and recorded before the first correction, because the tolerance left no room for improvised strokes. Intermediate inspections after each stage caught deviations while they were still correctable, instead of inspecting defects in afterwards.
The Result: 0.05 mm as Required
Arbetsstyckets rakhet efter uträtning reached 0.05 mm, on the mark of the client’s requirement. How that number was measured is documented in the verification section below.
The client expressed satisfaction with the results and interest in future collaboration. The transferable engineering lessons are summarized in the final section of this article.
Ser framåt
This case is one sample lot on one workpiece family; the sections above record what was measured and what carried the result. The next project starts from the drawing and its tolerance callout, not from this narrative.
How a Result Like This Is Verified Rather Than Declared
A straightness result at the 0.05 mm level is a joint property of the part and the measurement system, so the verification chain is what makes the number meaningful. The chain that supports a claim of this class runs: an agreed datum and support condition, written into the inspection instruction; a gauge whose repeatability on this part family has been demonstrated — because at tight tolerances the gauge’s own scatter is a visible fraction of the limit, the discipline of gage R&R för att räta ut linjer is not optional; released-state measurement after correction force is fully removed, per loaded versus released practice; and correlation to the customer’s own reference method on matched parts, so both sides of the shipment read the same part the same way. Within that chain, a supplier’s internal reading and the customer’s acceptance gauge agreeing is the result — the individual number on either instrument alone is only an interim.
What Transfers From This Case to Other Workpieces
The specific workpiece belongs to one client, but the engineering pattern repeats across families. Första: on stepped or tapered slender parts, build the correction plan around the stiffness map, not the single worst reading. Andra: fix the datum definition with the customer before any trial stroke, and prove its repeatability with reseating checks. Tredje: treat functional surfaces — flutes, skärkanter, finishing zones — as protected zones with explicit contact rules, in the discipline shared with stepped medical drill straightening och small-diameter medical drill applications. Fourth: let the acceptance evidence — released-state measurement on the agreed gauge, with rework limits and disposition defined in advance — be the arbiter, not the optimism of the production floor. Parts that follow those four rules converge in fewer strokes and survive audit; parts that skip them consume rework budgets learning the same lessons again.
FAQ
Why do stepped shafts bend near the diameter transitions?
Because stiffness changes abruptly at each shoulder. Stress from handling, heat treatment and prior machining concentrates where the section changes, and the transition acts as a hinge under any later load. Correction plans for stepped parts therefore map the shoulders explicitly and place press points with the stiffness map in view, rather than assuming a uniform rod.
är 0.05 mm straightness limited by the machine or the measurement?
At that level, both matter and the measurement usually dominates the conversation. The gauge’s own repeatability is a visible fraction of the tolerance, so the datum, support condition and gauge capability must be demonstrated before any correction result can be interpreted. This is why tight-tolerance projects front-load the measurement work.
Can flute zones be used as contact points during correction?
Generally not. Flutes and cutting edges are functional surfaces, and contact there risks edge damage that no straightness gain justifies. Correct practice places supports and press contact on the plain shank or agreed non-functional zones, with tooling geometry that spreads the load — the contact-zone discipline shared across tool straightening applications.
If this is your first drill bit straightening line, read the straightener selection walkthrough first, then benchmark your budget against the acceptance test checklist for a new machine.